homepage
Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit
banner
Home

nanocrystalline

nanocrystalline

  • Solid State Transformer Magnetic Components Explained: Cores Inside SST Power Stages
    Solid State Transformer Magnetic Components Explained: Cores Inside SST Power Stages
    Sep 28, 2026
    Which cores sit inside an SST power stage? Solid state transformer (SST) magnetic components are the high- or medium-frequency transformers, filter inductors, and EMI chokes that enable power conversion stages to replace bulky line-frequency magnetics. Inside an SST, cores see elevated switching frequencies, multilevel or modular converter stresses, isolation requirements, and thermal density that differ from 50/60 Hz distribution transformers. Nanocrystalline and amorphous alloys often appear in medium-frequency transformers and high-performance filters because of favorable loss/size trade-offs and high Bs (~1.25 T class for iron-based nanocrystalline vs ~0.4 T ferrite), while ferrite remains relevant in some higher-frequency, lower-flux niches. Specify cores by stage function—isolation transformer, link inductor, or CMC—not by a single “SST alloy” slogan. SST magnetics by stage role From a magnetics desk, SST architecture usually breaks into: Input stage — AC/DC or multilevel conversion with line filters (CMCs, DM inductors) Isolation stage — medium/high-frequency transformers (the heart of size reduction) Output stage — inversion or DC ports with additional filter magnetics Auxiliary magnetics — gate-drive transformers, sensors/CTs, snubber inductors Each block has different flux, frequency, and insulation demands. Buying “one core material for the SST” is how programs stall. JH has already published focused content on SST size-versus-heat at 50 kHz and a 24 MW SST nanocrystalline architecture note; here we map component roles and core selection questions so OEM buyers and applications engineers share vocabulary when requesting samples. Isolation / medium-frequency transformer checklist: target frequency band and waveform (square, quasi-square, multilevel); voltage-second product and ΔB budget; isolation voltage, partial discharge, creepage/clearance on the finished winding; thermal path (oil, air, cold plate, potting); mechanical geometry suited to the winding scheme. Material family Typical SST-leaning role Watch-outs Nanocrystalline Medium-frequency isolation & high-performance filters Ribbon insulation, cutting, AL control Amorphous Competitive loss/size in defined bands Noise, cutting, grade selection Ferrite Higher frequency / lower flux designs Temp derating near ~100–120°C class; Bs ~0.4 T Silicon steel Lower frequency / large power traditional Not the SST miniaturization story Nanocrystalline Curie ~570°C helps magnetically at elevated temperature; finished systems still face copper and insulation limits. SST insulation systems may differ from PSU case windows (-40 to +140°C discussions elsewhere) and must be specified explicitly. Filter inductors and link magnetics: Boost / buck / resonant tank inductors depending on topology; DM chokes on AC ports; CMCs for EMI against grid codes. Inductor cores should be inductor-oriented grades with AL vs DC bias honesty—not high-μ CMC grades pressed into energy storage (the μ trap). Gapped designs need fringing hotspot discipline for copper near gaps. Grid-connected SSTs face strict harmonic and EMI expectations. High-μ nanocrystalline CMC grades (often ≈ 80,000–190,000 class) help when high current and strong low-frequency CM impedance are required. Complement—not rewrite—your CMC selection process: size by impedance band, current, and temperature. Cut nanocrystalline C-cores appear in SST isolation and high-frequency transformer stages. Stresses, comparison, and RFQ discipline SST modules may see fast dv/dt from SiC/GaN stressing insulation; common-mode voltages across isolation transformers; uneven module loading in cascaded architectures; wide ambient in outdoor energy cabinets. Core RFQs should include insulation system questions (ceramic vs organic ribbon themes), hi-pot strategy, and thermal mapping—not only Ae and AL. Stage magnetics Primary job Core selection focus Failure if mismatched MF/HF isolation transformer Energy transfer + isolation Loss vs f, ΔB, insulation Overheat, PD, bulk Link / filter inductor Energy storage / ripple AL under bias, fringing Saturation, hot copper Line CMC CM EMI impedance High μ, current, temp EMC fail when hot/loaded CT / sensors Measurement Accuracy, burden, temp Control error Gate-drive transformer Isolation for gates Capacitance, creepage Shoot-through risk Thermal and mechanical: Measure winding and core temperatures under worst multilevel patterns—not only sinusoidal lab excitation. Magnetostriction audible noise can appear in outdoor installations. Vibration in mobile or trailer-mounted systems needs impregnation and mount control. Do not assume liquid cooling of semiconductors cools every magnetic component equally. RFQ template: “Component role: [MF transformer / CMC / DM inductor / CT]. Topology frequency ___ kHz; waveform notes ___; voltage-second or L(I) targets ___; isolation voltage ___; ambient/hotspot ___; cooling method ___; preferred alloy family ___; documentation (ISO/IATF) ___; annual volume ___.” Development sequence: Freeze architecture frequencies and modularity → allocate loss budgets per magnetic component → select materials per role and prototype transformers and filters separately → integrate EMI early (SST cabinets are excellent antennas when leakage is ignored) → only then optimize cost with tooling and PPAP if automotive-adjacent. Skipping EMI early creates late shields and capacitor banks that erase earlier size wins. Appoint a magnetics owner who translates volt-seconds into ΔB and Ae candidates, isolation specs into winding/core insulation asks, cabinet airflow into hotspot limits, and EMC pre-scan results into CMC vs DM actions. In modular SSTs, shared AC-port CMCs see aggregated EMI of many cells—undersizing them is a common system mistake when each cell team only budgets “its own” noise. Tag each BOM line with role and grade family so warehouse staff cannot interchange parts by OD. Dongguan JH Amorphous supplies OEM/ODM nanocrystalline and amorphous cores (ISO9001:2015, IATF 16949) for energy and industrial power electronics teams building SST-like architectures. SST magnetics mix closed toroids and cut cores depending on energy storage vs isolation needs. Filter-stage wound magnetics: size by role (CMC vs DM), not by a single SST alloy slogan. Closed-path toroids for CM filtering alongside cut cores for isolation stages. FAQ Q1: Is nanocrystalline always required for SST transformers? No. It is a strong candidate for many medium-frequency designs, but frequency, voltage, and cooling can favor other families. Compare loss and insulation readiness. Q2: Can ferrite SST transformers work at high power? Sometimes at higher frequency and carefully managed flux/temperature. Bs ~0.4 T and thermal derating near ~100–120°C class behavior limit some dense designs. Q3: Do SSTs still need common mode chokes? Usually yes at AC interfaces and often on other ports. Electronics do not remove EMI physics. Q4: What is the first datasheet trap in SST magnetics buying? Using CMC high-μ permeability rows to specify power inductors or transformers without loss and bias data. Larger core windows for higher power SST stages—loss density and cooling paths dominate sizing. Related reading Engineering the 50 kHz SST size-vs-heat trade-off 24 MW SST design with nanocrystalline cores Amorphous vs nanocrystalline for EVs and PV High-power nanocrystalline cut C-core If you need OEM core samples by SST stage role, email julia@amorphousoem.com with frequency, isolation, and thermal targets — www.amorphousoem.com.
    Read More
  • Open Magnetic Path EMI Signatures: How Leakage Fields Show Up on EMC Scans
    Open Magnetic Path EMI Signatures: How Leakage Fields Show Up on EMC Scans
    Sep 26, 2026
    How do leakage fields show up on the EMC scan? Open magnetic path EMI signatures appear when flux is not confined inside a high-permeability closed core—because of gapped inductors, poorly canceled windings, rod-like open structures, or leakage from CMCs—and that escaping field couples into cables, PCB loops, and chamber antennas. On EMC scans you often see broadband or harmonic-rich elevations that change dramatically when you move a near-field probe around the magnetics or slightly relocate a harness. Fixing capacitors alone rarely solves it: you need magnetic path control, winding symmetry, layout distance, and sometimes shields—plus the right nanocrystalline or ferrite core strategy for the filter role. Start from the CMC selection guide when the part is truly CM duty. Cased closed-path CMCs: flux stays in the core. Open-path or poorly canceled turns leak onto nearby loops. Closed path vs open path on the bench A toroidal high-μ nanocrystalline CMC aims for a closed magnetic path: common-mode ampere-turns drive flux in the core; differential current largely cancels. An open path (intentional gap, rod core, incomplete cancellation, large leakage) stores or leaks energy outside the core volume. Leakage fields are useful (transformer isolation, some sensors) and harmful (EMI, heating of nearby metal, acoustic vibration). EMC labs see the harmful side as conducted noise that looks immune to Y-cap tweaks, radiated hotspots near magnetics, and failures that appear only with production cable routing. Observation Suggests Near-field probe peaks at gap or rod ends Fringing / open path radiation EMI changes when rotating a toroid CMC Leakage / winding asymmetry Fail band tracks f_sw harmonics Switching magnetics coupling Touching chassis near inductor shifts plot Field into structure currents Cut / gapped cores: the open magnetic path is intentional for energy storage—and it is also where EMI probes light up. CM vs DM roles. CMCs have intentional or parasitic leakage inductance that can help differential filtering—but excess leakage and poor winding symmetry radiate and convert modes. High-μ nanocrystalline CMCs (μ often ≈ 80,000–190,000 for CMC grades) are excellent closed-path CM impedances when wound correctly; they are not automatic EMC insurance if lead dress creates large loops. Gapped DM inductors must leak by design. That fringe is where copper hotspots and EMI pickup coexist—see the fringing loss notes. Treat gap orientation as an EMC orientation problem, not only a thermal one. Reading the scan like a magnetics engineer Identify whether the fail is conducted, radiated, or both. Use a near-field probe map before ordering more capacitors. Correlate peaks to f_sw, burst modes, and PFC harmonics. Temporarily add distance between suspect magnetics and harness—if the plot improves a lot, path/leakage is implicated. Check winding start/finish and twist of CMC leads. Only then change core material, AL, or add shields. This order prevents expensive core swaps when a 20 mm cable move was the real fix. Design controls that reduce open-path EMI Magnetic design. Prefer closed-path CMCs for CM noise; use nanocrystalline when high current + strong low-frequency CM impedance is needed (Bs ~1.25 T class headroom vs ferrite ~0.4 T). For gapped DM parts, minimize unnecessary loop area and keep fringe away from sensitive nets. Avoid treating open rods as filters next to long cables without a shielding strategy. Layout. Short, tight CMC lead pairs. Keep noisy switch nodes away from magnetics that can re-radiate. Mind return paths under inductors on multilayer PCBs. Mechanical. Gap mark orientation standardized in assembly. Metal brackets can be useful shields or accidental shorted turns—validate. System. Cable common-mode chokes at panel entry when cabinet coupling dominates. Keep grounding philosophy consistent with safety and EMC. Ferrite may derate as temperatures approach the ~100–120°C discussion zone; nanocrystalline Curie ~570°C and finished assemblies often discussed from about -40°C to +140°C change the thermal EMI story. Neither material removes the need for closed-path thinking. An open-path ferrite and an open-path nanocrystalline can both fail radiated tests if layout ignores leakage. Dongguan JH Amorphous supports OEM/ODM cores for CMCs and inductors under ISO9001:2015 and IATF 16949. Match closed-path CMC grades vs inductor grades so EMI roles stay clear. Approach When it helps When it fails More X/Y capacitors True CM/DM impedance gaps Leakage coupling / loop antennas Snubbers Switching edges Not a substitute for open-path control Shield cans Local radiated Thermal & capacitive side effects Closed-path CMC upgrade High CM current, hot, LF EMI Wrong if problem is DM gap radiation only Cable routing / twist Harness pickup Ignores on-board fringe Mode conversion. Leakage and imbalance convert differential switching energy into common-mode currents on cables. That is why a “DM-only” inductor problem becomes a conducted CM fail on the LISN. Symmetry, tightly paired returns, and correct CMC placement after the noisy node are essential. Pre-compliance checklist. Photo of gap orientation vs cable exit CMC winding sense and lead length documented Near-field map at f_sw and 2nd/3rd harmonics Hot EMI scan after thermal soak if ferrite is in the path Confirm magnetic grade matches role (CMC vs inductor) Note any metal bracket acting as a turn Change the core when AL, saturation, temperature derating, or CM impedance is truly insufficient Change the drawing when orientation, keep-outs, and lead dress are uncontrolled Wound toroids on the bench: lead dress and proximity to harnesses often move the EMC plot more than another capacitor. FAQ Q1: Does higher permeability always reduce leakage EMI? Higher μ helps confine flux in a closed core for CM magnetization, but winding asymmetry and external loops still radiate. Gapped inductors will always fringe. Q2: Can I use a CMC core as a gapped DM inductor to save SKUs? Magnetically unwise—different grades and purposes. See high-μ vs low-μ datasheet guidance. Q3: Why does my EMI fail only with the production harness? Harnesses form antennas and return paths that lab pigtails omit. Leakage fields need those antennas to show up. Q4: What should I send a core supplier when EMI implicates magnetics? Fail bands, topology, currents, photos of magnetics orientation, and whether the part is CM or DM duty. High-volume casing lines: mechanical consistency of the case also affects leakage and mounting geometry. Related reading Common mode choke selection guide Mastering EMI suppression Air-gap fringing loss (gap radiation / copper) Is common-mode noise sabotaging your circuit? If an EMC plot seems to blame the toroid, send fail bands and magnetics photos to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Air-Gap Fringing Loss: Why Copper Hotspots Sit Next to the Gap (and How to Place Windings)
    Air-Gap Fringing Loss: Why Copper Hotspots Sit Next to the Gap (and How to Place Windings)
    Sep 23, 2026
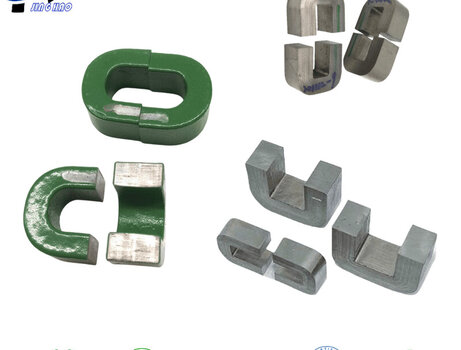
    Why is the copper next to the gap always the hotspot? Air-gap fringing loss appears when the magnetic field bulges out of a discrete gap and cuts nearby copper, inducing extra eddy-current heating. That is why thermal cameras often show winding hotspots immediately adjacent to the gap—even when average current density looks safe. Reduce the problem by keeping copper out of the strongest fringe, using spacer/coil architectures that distance the first turns, considering distributed or carefully shaped gaps, and verifying both loss and inductance under DC bias. Material choice (ferrite, amorphous, nanocrystalline) still matters for Bs and temperature, but winding geometry next to the gap frequently dominates local hotspots. Why fringing exists and where it heats An air gap stores energy by lowering effective permeability and linearizing AL under DC bias. The field does not stop abruptly at the gap edges: flux fringes into the winding window. Consequences: local H and B outside the intended gap volume; AC field components cutting copper strands → eddy losses that scale badly with frequency and strand diameter; proximity-effect aggravation in nearby layers; mechanical forces that contribute to acoustic noise. For OEM power inductors in PFC stages, DC–DC bricks, and differential-mode chokes, fringing is everyday gapped design—not a corner case. LocationWhy it runs hotMitigation theme Turns hugging gap facesStrongest fringe cuts copperKeep clearance; use slot bobbins Inner layer near gap on cut toroidConcentrated bulgeOffset winding, spacer Thick Litz bundle in fringeStrand eddySmaller strands, move bundle PCB copper under gapped ER/PQField into planeCutouts, distance Fringing loss vs classic copper I²R: Design reviews sometimes blame “not enough copper” when IR drop is fine but the hotspot is brutal. Split the budget: (1) DC I²R from I_rms and resistance; (2) skin and proximity in the winding volume generally; (3) fringing-induced eddy localized where gap flux escapes. Item (3) can dominate a small region, raising local temperature enough to discolor enamel while average winding rise looks acceptable. Rule-of-thumb notes (refine with FEA or experiment): fringing influence extends on the order of the gap length into the window—treat “several gap lengths” as a keep-out intuition. Higher f_sw and larger strand diameter in the fringe make eddy heating worse. Increasing gap to hold L under bias can improve magnetic linearity yet worsen fringe heating—trade explicitly. Nanocrystalline and amorphous gapped cores used for high-current inductors—including PFC inductor cores—can run substantial AC flux. Bs headroom (~1.25 T class for iron-based nanocrystalline vs ~0.4 T ferrite) helps size, but copper next to the gap still needs respect. Treat core shape and gap method as the technical distinction—not casual shape nicknames. Cut C-cores make the gap explicit: fringing fields leave the cut faces and heat nearby copper. How to place windings on gapped cores Cut / gapped toroid: Identify gap location on the finished core. Leave a copper-free sector around the gap when the design allows. Start winding away from the gap; use tape or spacer to enforce distance. Prefer Litz appropriate for f_sw, but do not park a thick bundle in the fringe to fill the window. For production, document winding start angle relative to the gap mark so every operator repeats the thermal result. Bobbin cores (PQ, E, ER): Use coil geometries that recess the first winding layer from the gap centerline. Watch foil windings: wide foils are efficient for DC but can act as eddy sails in fringe—slotting or distancing may be required. Thermal vias and potting help only if heat can leave; they do not remove the eddy source. Distributed gap approaches: Distributed gaps reduce peak fringe intensity compared with one large discrete gap, often improving copper temperature at the cost of different loss and cost structures. Evaluate on your f_sw and current; do not assume “distributed always cooler” without measurement. Dongguan JH Amorphous supplies OEM/ODM nanocrystalline and amorphous cores (ISO9001:2015, IATF 16949). For inductor grades we emphasize AL vs DC bias, loss orientation, and manufacturing marks that help winding houses avoid the gap hotspot. Product mix showing cut cores beside closed toroids—gap policy belongs in the RFQ, not as an afterthought. Design workflow and production drift Set L(I) requirement—define I_sat and I_rms. Choose gap / effective μ strategy—discrete vs distributed. Estimate copper loss without fringe; then add experimental margin or FEA for the gap region. Prototype with a thermal camera focused on gap-adjacent copper. Iterate winding distance and stranding before enlarging the core as a first move. Re-check EMI and acoustics—gap and winding changes affect leakage and noise (and can feed inductor whistle if ΔB sits in the audio band). LeverProsCons Increase clearance to gapFast, low tooling costMay reduce turns window Finer Litz in fringe zoneCuts eddy in hotspotCost, fill factor Split/distribute gapLower peak fringeProcess complexity Larger AeLower ΔB & densitySize, cost, weight Lower f_swLess AC eddySystem-level impacts The cheapest watt saved is often a few millimeters of winding offset. Control-plan items for gapped cores: gap length tolerance; visual gap mark relative to case; AL window at stated DC bias points; ribbon insulation integrity after cutting; cleanliness (metal fines must not bridge turns). Prototype-to-mass drift: hand-placed spacers omitted later; Litz strand diameter change; varnish change; clamp force shifting copper into the fringe; firmware raising f_sw without revisiting fringe eddy. After a thermal fix, re-run conducted EMI and update the BOM so purchasing cannot “equivalent” a core with a different gap-mark scheme. Cased closed cores avoid discrete gaps; when you do gap, plan winding clearance for fringing hotspots. FAQ Q1: Does fringing change the effective inductance? Yes. Fringing increases effective gap area somewhat, raising AL slightly versus a naïve gap formula. Calibrate AL on the real core. Q2: Are nanocrystalline gapped cores worse for fringing than ferrite? Fringing is geometric. Nanocrystalline’s higher Bs can shrink size and raise field density if you push miniaturization, which can intensify local problems—design responsibly. Q3: Can I shield the gap with copper tape? A shorted shield in the fringe can itself heat and may alter inductance. Use carefully and measure; it is not a free thermal fix. Q4: What should RFQs include? Gap specification, AL vs bias, preferred winding keep-out, f_sw, I_rms/I_peak, and a request for gap location marking for manufacturing. Related reading Why power inductors whistle (magnetostriction) The μ trap on nanocrystalline datasheets Amorphous cores for PFC inductors Nanocrystalline cores for power applications If a thermal camera shows copper hot next to the gap, send gap length, f_sw, and current targets to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Why Your Power Inductor Whistles: Magnetostriction vs Thermal Noise in Soft Magnetic Cores
    Why Your Power Inductor Whistles: Magnetostriction vs Thermal Noise in Soft Magnetic Cores
    Sep 22, 2026
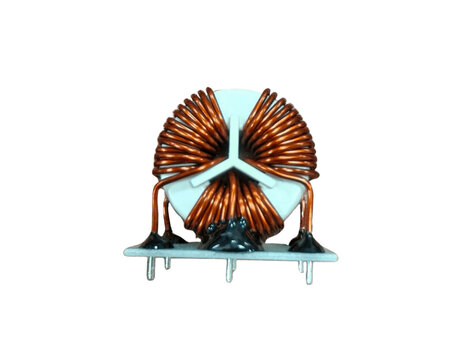
    Is that whistle magnetostriction or something else? A power inductor “whistle” is usually audible magnetostriction or mechanical vibration driven by magnetizing force at audio-band frequencies—not random thermal hiss. Soft magnetic cores strain slightly with flux (magnetostriction). If drive frequency, harmonics, or beat notes fall near 2–20 kHz, the assembly radiates sound. Thermal effects change expansion and varnish damping; they rarely create a pure tone alone. Fix the root: reduce ΔB in the audio band, avoid discontinuous magnetizing patterns that create tones, damp the mechanical stack, and select inductor-oriented grades (nanocrystalline or amorphous) with noise and loss in mind—not only AL and Bs. Diagnose before you swap the core Field returns that say “the magnetics sing” mix several mechanisms: Magnetostrictive acoustic emission — dimensional change with B, coupling into case, PCB, and chassis. Lorentz / winding forces — conductors in leakage fields vibrate at twice line frequency or at switching-related tones. Mechanical buzz — loose gaps, clips, varnish voids, or mounting resonance. True thermal (Johnson) noise — broadband and tiny; almost never the tonal whistle heard across a lab bench. SymptomLikely dominant causeFirst checks Pure tone tracking f_sw or f_sw/NMagnetostriction / magnetic forceΔB, DCM/CCM boundary, burst mode Tone at 100/120 Hz or multiplesLine-frequency magnetics / LorentzRectifier ripple, mounting, clamps Rattle changing with tap testLoose mechanical stackGap filler, varnish, clip torque Broadband hiss, no loud toneElectrical noise / EMI pathNot a core whistle problem Replacing a core “because it is noisy” without checking excitation frequency and mounting often moves the tone instead of removing it. Physics that matters for buyers: sound power scales with flux swing and mechanical coupling, not with μ alone. Burst-mode, skip-cycle, and light-load regimes often push energy into audible bands even when full-load operation is quiet. Gapped inductors add fringing; fringing increases local copper force and vibration paths next to the gap. Case, epoxy, and mounting can damp or amplify. Iron-based nanocrystalline materials offer Bs ≈ 1.25 T and usable temperature windows that support compact designs. Compactness raises ΔB if turns and Ae are pushed hard. Noise control belongs in the magnetic design review, not only in the enclosure review. FactorMn-Zn ferriteAmorphousNanocrystalline Bs (typical order)~0.4 THigh (alloy-dependent)~1.25 T Audible risk driverΔB & burst modesMagnetostriction + mountingMagnetostriction + high ΔB if over-miniaturized High-temp holdDerates near ~100–120°C classApplication-dependentCurie ~570°C; finished cases often −40 to +140°C Design leverLower ΔB, avoid burst tonesDamping, grade, impregnationGrade/finishing, ΔB, impregnation, mount No material is always silent. Excitation and mechanics dominate. Copper on a toroid can couple magnetostriction into audible vibration—diagnose before you change the core chemistry. Thermal–mechanical effects vs “thermal noise” “Thermal noise” in electronics usually means Johnson noise—irrelevant to a whistling choke on a bench. What people often mean: Temperature-driven dimensional change altering clamping force and resonance Varnish Tg / softening changing damping as the inductor warms Differential expansion between copper, core, and plastic case creating buzz after soak Those modulate an existing magneto-mechanical drive. They do not replace magnetostriction as the tone generator. Cold start: stiff varnish, higher mechanical Q → sharper tone possible. Warm operation: damping may rise or fall with the resin system. Hot spot near a gap: local copper expansion and force concentration. Automotive cold (−40°C class) vs under-hood heat: mount stiffness changes. Spec acoustic checks at min, typical, and max temperature—not only at 25°C lab air. Coated power-inductor toroid: coating and case stiffness change how vibration reaches the PCB. Design levers that cut whistle Magnetic excitation: Prefer continuous conduction strategies that avoid audio-band burst patterns when product requirements allow. Reduce ΔB with more turns, larger Ae, or lower voltage-second product. Spread spectrum or shift frequencies out of peak ear sensitivity only when EMI and control allow—then revalidate EMC. Avoid operating near saturation corners where magnetizing-current distortion creates strong harmonics. Select inductor-oriented grades (controlled effective μ under bias)—not a high-μ CMC core pressed into energy-storage duty (μ trap explained). Core finishing and mechanics: Discuss impregnation, varnish, and case damping with your core OEM. For gapped parts, treat the gap region as both a thermal and acoustic hotspot—see also air-gap fringing loss and winding placement. Use rigid, damped mounting; avoid cantilevered heavy magnetics. Potting can damp vibration but may raise thermal resistance—validate both. Lab sequence: Capture inductor current and a microphone channel on the same DAQ. Sweep load from no-load to full, including firmware modes sales demos never show. Note core-case and winding temperatures. Repeat with a soft pad under the board to separate structure-borne contribution. Change one magnetic variable at a time (gap, turns, grade, varnish). EV charger light-load night charging and server acoustic contracts are common failure contexts: burst PFC or LLC skip modes create household-audible tones even when full-load EMI passes. Ask for light-load acoustic acceptance in the DV plan. Dongguan JH Amorphous supports OEM/ODM nanocrystalline and amorphous cores under ISO9001:2015 and IATF 16949. We do not promise a universal silent alloy; we match grade, AL under bias, and finishing to your excitation and mounting reality. Epoxy-coated nanocrystalline rings used in inductor and CMC builds where acoustic limits matter. FAQ Q1: Is magnetostriction the same as core loss? No. Core loss is energy dissipated as heat from hysteresis and eddy currents. Magnetostriction is strain. They can correlate with excitation, but fixing loss does not automatically fix sound. Q2: Will a higher-μ nanocrystalline core whistle less? Not necessarily. Higher μ may reduce turns for a target L at low bias, but a CMC-oriented high-μ grade used as a power inductor can worsen harmonics via saturation. Match grade to inductor duty. Q3: Can thermal noise explain a loud 6 kHz tone? Almost never. A loud pure tone is magneto-mechanical or mechanical. Thermal noise is broadband and tiny. Q4: What should I put on an RFQ if acoustics matter? State max SPL or “no audible tone at 1 m in quiet room” across load/temperature, list firmware modes, and request inductor-grade cores with impregnation options—not only OD and AL. Related reading Air-gap fringing loss and winding placement The μ trap: high-μ CMC vs low-μ inductor grades High-temperature magnetics comparison PFC inductor amorphous cores If a prototype inductor is whistling and you want a second look at grade and excitation, send I_L / V notes to julia@amorphousoem.com — www.amorphousoem.com.
    Read More

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

home

products

WhatsApp

Contact