homepage
Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit
banner
Home

Blog

Blog

  • Ferrite vs Nanocrystalline Cores for EMI and CMC: When Each Wins (and What to Freeze Before You Switch)
    Ferrite vs Nanocrystalline Cores for EMI and CMC: When Each Wins (and What to Freeze Before You Switch)
    Sep 30, 2026
    Ferrite and nanocrystalline are not drop-in twins If you design EMI filters or power magnetics for industrial, EV, or server-class PSUs, you have lived this choice: MnZn/NiZn ferrite on one side of the bench, iron-based nanocrystalline ribbon cores on the other. Brochure tables make the swap look obvious—higher Bs, higher μ, “better EMI.” On a real CMC or inductor drawing, the materials behave differently under bias, temperature soak, and AL fixture correlation. That gap is exactly where dual-source programs either land cleanly or reopen EMC after SOP. This article is written for high-spec buyers in JP, CA, US, FR, UK, IT, RU, and similar markets who already ran VAC Vitroperm-class or Hitachi Metals Finemet-class nanocrystalline programs and now need a China OEM as engineering second source—not a cheap catalog substitute. Dongguan JH Amorphous Co., Ltd. (www.amorphousoem.com) supplies OEM/ODM amorphous and nanocrystalline cores under ISO9001:2015 and IATF 16949. We help freeze grade intent, AL/Z windows, and change control so a second source supports your filter, not quietly rewrites it. What each material actually is (in magnetics terms) Ferrite is a sintered ceramic (iron oxide plus Mn/Zn or Ni/Zn oxides). High resistivity keeps eddy currents low; shapes are moldable (toroids, E/U cores, beads). MnZn grades are the usual workhorse for power and mid-band EMI; NiZn typically pushes higher frequency at the cost of lower μ. Saturation flux density for common MnZn CMC grades sits roughly in the ~0.3–0.5 T neighborhood. Curie temperatures are relatively low, so permeability and loss can move hard as the hotspot approaches ~100–120°C—see high-temperature magnetics when ferrite derates. Nanocrystalline starts as rapidly solidified Fe-Si-B-Nb-Cu (and related) amorphous ribbon, then anneals into ~10–20 nm grains. Finished cores are usually cased or coated toroids / cut cores. Typical iron-based grades used in CMCs offer Bs around ~1.2–1.25 T class, very high initial permeability (often discussed as tens of thousands to >80,000 depending on grade and test conditions), low magnetostriction, and alloy Curie near ~570°C. The finished assembly still lives inside copper enamel, case polymer, and varnish limits—often discussed about -40°C to +140°C for the wound part. High-μ CMC grades and lower-μ energy-storage / inductor-oriented finishes are different anneal philosophies; mixing them by OD alone is the classic μ trap. Coated ribbon cores — finish and insulation belong on the drawing with grade, not as an afterthought. Comparison table: EMI / CMC / power magnetics tradeoffs Numbers below are order-of-magnitude engineering neighborhoods for discussion—always lock AL or impedance at your frequency, excitation, and fixture. Do not treat trademark alloy families as interchangeable by name; when buyers say “VAC/Finemet-class,” translate into measurable windows on the drawing. Property / decision Ferrite (typical MnZn CMC / power) Iron-based nanocrystalline (CMC-class) Composition Ceramic oxide (MnZn / NiZn) Metallic ribbon alloy (Fe-Si-B-Nb-Cu class), annealed Bs (order) ~0.3–0.5 T ~1.2–1.25 T class Initial μ (order) ~1,500–15,000 (grade-dependent) Very high (often >> ferrite; grade & test condition driven) Useful EMI band (CMC practice) Strong mid–high MHz; NiZn for HF beads Strong from tens of kHz into several MHz; broadband CM impedance Thermal / Curie story Softens near ~100–120°C hotspot class Alloy Curie ~570°C; assembly limited by Cu/case (~-40 to +140°C class) Core loss / size Higher loss → larger stack for same EMI/thermal Lower loss, fewer turns, smaller volume for high-current CM Mechanics Brittle ceramic; moldable shapes Thin ribbon; needs case/varnish; winding stress matters Relative piece cost Usually lower Higher unit price; often lower system EMI/thermal cost When it wins Modest current, cool ambient, HF-only noise, cost-sensitive SMPS High CM current, low-frequency EMI, hot EMI soaks, size-constrained OBC/inverter For choke sizing practice—AL, OD/ID/HT, casing, and impedance bands—use the common mode choke selection guide. Product-family context for wound CMC cores: nanocrystalline common mode choke cores. Cased nanocrystalline CMC cores — high Bs and high-μ grades for low-frequency / high-current common-mode stages. When ferrite still wins Nanocrystalline is not a blanket upgrade. Ferrite remains the right call when: Noise is high-frequency and current is modest. NiZn beads and small MnZn CMCs often cover MHz-range conducted/radiated issues without paying for high Bs. Hotspot stays cool. If thermal mapping shows the core well below the ferrite soft region, μ collapse is not your limiter—copper or layout may be. Shape and gap freedom matter more than Bs. Complex E/U geometries, adjustable gaps, and multi-gap stacks are mature in ferrite tooling. Cascade filters already mix materials. Many industrial EMI stages use ferrite on the HF end and nanocrystalline on the low-frequency / high-current CM stage. Replacing both with one alloy because of a brochure is rarely optimal. Cost-only consumer SMPS with loose EMI margin where requalification risk is low and ambient is gentle. Related material discussion: how core materials define CMC performance. When nanocrystalline (VAC / Finemet-class performance neighborhood) wins Use nanocrystalline when the failure mode is saturation under CM surge / bias, insufficient impedance below a few hundred kHz, or EMI that collapses after a hot soak on ferrite. Typical contexts: EV onboard chargers and DC-DC front-ends, high-power industrial inverters, compact UPS/server PSUs, and multi-frequency noise where fewer turns and higher Bs shrink the filter. Bs headroom (~1.25 T class vs ~0.4 T ferrite) lets you hold inductance under peak current that would drive ferrite soft. Language discipline for RFQs: say VAC/Finemet-class or comparable grade when you mean a performance neighborhood (high-μ CM vs inductor finish, Bs/thermal story, AL window). Do not claim trademark equivalence or identical chemistry unless your lab and legal teams have that evidence. Most dual-source programs prove fit-for-function on the wound CMC or inductor against an incumbent sample. Checklist depth: second-sourcing nanocrystalline cores—what VAC/Finemet-class buyers should freeze. Saturation, permeability, and thermal—what actually breaks EMI Saturation. Ferrite’s lower Bs means CM surge or DC bias collapses μ earlier; the choke looks fine at light load and fails under load dump or motor start. Nanocrystalline delays that collapse, but an open magnetic path, poor lead dress, or wrong AL still fails EMC. Geometry mistakes are not fixed by alloy brand heritage. Permeability. Very high μ gives high CM impedance with fewer turns (lower copper loss), yet it is also easier to mis-apply: a high-μ CMC core pressed into gapped energy-storage duty, or an inductor-oriented grade sold into a CM filter, both look “nanocrystalline” on the PO and wrong on the spectrum analyzer. Freeze magnetic role on the drawing. Thermal. Ferrite derating near ~100–120°C is a magnetic story. Nanocrystalline’s high Curie is an alloy story; the wound choke still dies from enamel, case continuous-use temperature, or copper resistivity rise. Map hotspots, then decide whether μ/Bs collapse or assembly limits dominate. Insulation and casing choices belong in the same review as grade—ceramic vs organic ribbon insulation. Gapped inductor builds need winding keep-outs from fringe fields—air-gap fringing and winding placement. Second-source drawing freeze notes (before you switch materials or suppliers) Whether you move ferrite → nanocrystalline or dual-source a Finemet-/Vitroperm-class incumbent to a China OEM, freeze these items before samples leave the plant: Role: CMC (closed-path high-μ) vs inductor / PFC (gapped or lower-μ) vs CT—not “nanocrystalline toroid.” AL or Z window at stated frequency, excitation, and fixture notes; keep a golden sample for meter correlation. Geometry stack: OD/ID/HT, case type, gap mark, lead egress for the winding house. Insulation / coating / varnish system and what triggers a PCN. Thermal & EMI validation: wound-sample delta vs incumbent (conducted/near-field as applicable) after soak. QMS path: IATF scope when automotive, agreed PPAP level, change control—see IATF 16949 and PPAP for magnetic core suppliers. OEM core assortment — freeze role (CMC vs CT vs inductor) before OD alone drives the PO. Service-over-price buyers optimize requalification risk and field EMI, not piece price alone. A China second source that hits frozen AL histograms and PCN discipline is an engineering partner; a low quote that only matches OD is a future EMC reopen. Practical decision path List noise band, I_rms / I_peak CM, ambient and hotspot budget. If ferrite EMI fails after thermal soak or under surge—shortlist nanocrystalline CMC-class cores. If noise is HF-only and current/temperature are gentle—keep ferrite or cascade both. Size AL/Z and copper; verify on the wound part, not brochure μ. For dual source after VAC/Finemet-class history: freeze the drawing list above, then correlate samples. FAQ Q1: Can I drop a nanocrystalline toroid into a ferrite CMC footprint one-for-one? Sometimes on OD/ID/HT, rarely on electrical behavior without revalidating turns, AL, leakage, and EMI. Treat it as a design review, not a catalog swap. Q2: Is nanocrystalline always better for EMI? No. It usually wins on high-current / low-frequency CM and thermal stability of the magnetic function. Ferrite can still win at HF with modest current, or in cascade stages. Q3: What does “VAC/Finemet-class” mean in an RFQ to a China OEM? A performance neighborhood and incumbent correlation target—not a claim of trademark identity. Specify role, AL/Z conditions, geometry, insulation, and EMI/thermal delta expectations. Q4: Why did my ferrite CMC pass cold and fail after soak? μ and loss often move as ferrite approaches its soft thermal region (~100–120°C class). Re-map hotspot; consider nanocrystalline if magnetic derating is the limiter. Q5: What should purchasing and engineering freeze together? Grade intent (CMC vs inductor), AL/Z window with test notes, mechanical stack, insulation/PCN rules, and validation against the incumbent. Price alone should not reopen EMC. For ferrite-to-nanocrystalline reviews or VAC/Finemet-class second-source drawing checks (AL correlation, sample planning, CMC grade selection), contact julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Second-Sourcing Nanocrystalline Cores: What VAC / Finemet-Class Buyers Should Freeze Before Switching
    Second-Sourcing Nanocrystalline Cores: What VAC / Finemet-Class Buyers Should Freeze Before Switching
    Sep 29, 2026
    Why OEMs second-source nanocrystalline cores now Many power and EMI designs in Japan, North America, and Europe were frozen around well-known nanocrystalline brands—often discussed in the same breath as VAC Vitroperm-class or Hitachi Metals Finemet-class materials. Those programs still need high-μ CMCs, stable AL, and predictable EMI. What changed is supply strategy: dual source, shorter sample loops, and China OEM capacity that can hit engineering windows when drawings are written tightly. Second-sourcing is not “buy the cheapest toroid labeled nanocrystalline.” It is locking the magnetic grade intent, test conditions, and change control so a China manufacturer can support—not quietly rewrite—your filter or inductor. Dongguan JH Amorphous Co., Ltd. (www.amorphousoem.com) supplies OEM/ODM amorphous and nanocrystalline cores under ISO9001:2015 and IATF 16949. This article is a buyer/engineer checklist for second source and dual source programs aimed at service-sensitive markets (US, Canada, UK, France, Italy, Japan, and similar), not a price war playbook. Buyer priority What to freeze What fails if you skip it Role: CMC vs inductor Grade family (high-μ CM vs energy-storage / lower-μ) μ trap, wrong EMI or saturation behavior Geometry OD/ID/HT, case, gap mark, lead egress Winding house scrap, harness EMI AL / Z window Test frequency, excitation, fixture notes Lots that “pass OD” fail on the bench Quality system IATF scope, PPAP level, PCN rules Quiet process drift after SOP Validation EMI/thermal delta vs incumbent sample Field returns after dual-source swap Plastic-cased toroids: second-source reviews start with magnetic role and AL windows. VAC / Finemet-class language—without false equivalence Purchasing often says “VAC alternative” or “Finemet equivalent.” Engineering should translate that into measurable targets: permeability class for CM vs DM duty, Bs and thermal story vs ferrite, core loss at your kHz, dimensional stack for the winding house, and insulation/coating system. Trademarked alloy families are not interchangeable by name. Treat them as performance neighborhoods you reverse-engineer into a drawing. Claim “same brand chemistry” only when your lab and legal teams have that evidence—most second-source programs instead prove fit-for-function on the finished CMC or inductor. Useful framing for RFQs to China OEMs: Application: CMC / PFC inductor / cut C-core / CT—not “nanocrystalline toroid.” Incumbent sample available for AL correlation and EMI delta (preferred). Target AL or impedance band at stated conditions; reject “typical μ” as the only spec. Annual volume, sample lead time, and whether PPAP (or customer PPAP-like pack) is required. Contact path to applications engineering, not only sales. Related reading on the grade mistake that kills dual-source programs: the μ trap on nanocrystalline datasheets. For automotive paperwork depth, see IATF 16949 and PPAP for core suppliers. What to put on the drawing before you dual-source Magnetic role. High-μ closed-path grades for CM impedance are not the same anneal philosophy as gapped or lower-μ energy-storage cores. If the incumbent was a CMC, do not accept an “inductor-looking” nanocrystalline with a gap unless EMI and thermal are revalidated. Cut cores and fringing need their own keep-outs—see air-gap fringing and winding placement. AL / impedance. State frequency, waveform notes, and fixture correlation. Keep a golden sample when the second source uses a different AL meter. Lot histograms beat single-point brochure numbers. Mechanicals and insulation. Case resin, varnish, ceramic vs organic ribbon insulation, and edge condition affect hi-pot, thermal, and winding damage. Ask what changes trigger a PCN. Background: ceramic vs organic insulation questions for OEM buyers. Thermal and EMI context. Ferrite may be discussed as soft near ~100–120°C; nanocrystalline alloy Curie is far higher (~570°C class), but finished assemblies still live inside copper and plastic limits (often discussed about -40°C to +140°C). Open magnetic paths and poor lead dress still fail EMC regardless of brand heritage—open-path EMI signatures and high-temperature magnetics. Coated toroids across sizes: freeze the coating/insulation system when dual-sourcing an incumbent. Validation that service-focused buyers actually run Price-insensitive customers still hate requalification surprises. A practical second-source gate: Dimensional FAIR against the frozen drawing. AL / Z distribution on N pieces from the proposed production route. Wound sample: copper rise, acoustics if relevant, and near-field or conducted EMI delta vs incumbent. Thermal soak if ferrite was in the old path or ambient is hot. Paper: certificate scope page, control-plan outline, material declarations, agreed PPAP level for automotive. Field context from programs that already exercised nanocrystalline CMCs under real EMI/thermal pressure: German 800 V EMI case, Italian EV charger thermal/EMI case. Product examples to anchor RFQs: nanocrystalline cores for common mode chokes, cut C-cores for power magnetics, CMC selection guide. Market cue What they usually optimize Supplier behavior that fits US / CA / UK Drawing discipline, English FAE, dual source risk Clear AL windows, sample speed, PCN in writing DE / FR / IT EMC + automotive/industrial QMS IATF-aware packs, EMI delta data JP Consistency, packaging, communication quality Tight tolerances, lot codes, responsive FAE Other high-spec OEMs Second source without redesign Incumbent correlation, not catalog guesswork Oval / racetrack cores: lock window and build dimensions on the drawing, not just OD. Case and base options: resin, lead egress, and mounting belong in the change-control plan. Wound CMC assembly: prove fit-for-function with EMI and thermal delta against the incumbent. FAQ Q1: Can a China OEM replace a VAC- or Finemet-class core one-for-one? Sometimes on geometry and AL windows, never by trademark name alone. Prove fit-for-function on the wound part and freeze grade intent on the drawing. Q2: What is the fastest way to fail a second-source trial? Ordering by OD and “nanocrystalline” without CMC vs inductor grade, AL test conditions, or EMI delta against the incumbent. Q3: Do we need full PPAP for every dual-source core? Automotive serial parts usually yes at the agreed level; industrial programs still need a defined approval pack and PCN rules. Details: IATF/PPAP guide. Q4: Should we dual-source different anneal philosophies? Not without full requalification. Two routes that only share OD are two different parts electrically. Q5: Who should own the RFQ—purchasing or engineering? Both. Purchasing owns commercial dual-source risk; engineering owns magnetic role, AL, and EMI. JH Amorphous expects joint reviews so piece price does not reopen EMC. For second-source or dual-source nanocrystalline / amorphous core reviews (drawing check, AL correlation, sample planning), contact julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Common Mode vs Differential Mode Choke: How to Split Roles in Power Supply EMI Filters
    Common Mode vs Differential Mode Choke: How to Split Roles in Power Supply EMI Filters
    Sep 30, 2026
    How should CM and DM chokes split roles in the filter? A common mode choke (CMC) presents high impedance to noise currents that flow in the same direction on line and neutral (or on paired DC rails) while largely canceling flux for differential load current. A differential mode choke (DM choke) is an intentional series inductance in the power path that impedes normal-mode ripple and noise between the conductors. In power supply EMI filters you usually need both roles—often with X-capacitors for DM and Y-capacitors for CM—rather than forcing one part to do everything. Use high-μ nanocrystalline CMC grades for CM impedance at high current; use controlled-μ / gapped inductor-oriented cores for DM energy storage and ripple. For CMC sizing details, use JH’s published common mode choke selection guide. Why role splitting beats one big choke EMI failures mix CM and DM. Capacitor-only patches fail when inductance in the correct mode is missing. Conversely, oversized CMCs with huge leakage are sometimes asked to “also be the DM choke,” creating thermal, saturation, and radiated leakage problems. Role-split principles: Identify which mode fails on the LISN / EMC plot using separators, probes, or known X/Y sensitivity experiments. Assign CM impedance to a true CMC (closed-path, high μ, canceling windings). Assign DM impedance to DM inductors or to carefully budgeted CMC leakage—not accidental leakage alone. Match core grades to each role (avoid the μ trap). CMC role (pointer-style): CMCs suppress CM noise using high magnetizing inductance for in-phase currents. Iron-based nanocrystalline CMC cores typically offer Bs ~1.25 T, high initial μ (often ≈ 80,000–190,000 class for high-μ CMC grades), and stronger hot performance than ferrite that derates near ~100–120°C discussions, with finished assemblies often discussed from about −40°C to +140°C. Curie ~570°C for nanocrystalline alloys keeps the magnetic story viable when copper/plastics become the limiter. For step-by-step CMC selection (impedance band, current, AL, casing): see the published JH Common Mode Choke Selection Guide. This post does not rewrite that guide. CMC checklist: winding sense creates flux cancellation for DM current; lead dress stays tight to avoid turning the CMC into an antenna; imbalance and surge ampere-turns considered so μ does not collapse when you need it; temperature soak included in EMI proof. DM choke role: DM chokes see the full load current as magnetizing current (no cancellation). Therefore effective μ must be controlled so L holds under DC or low-frequency line current; gaps or distributed-gap strategies are common; fringing fields heat nearby copper and can radiate—manage winding placement; core loss and copper loss both matter at ripple frequencies. Use nanocrystalline or amorphous inductor-oriented grades—not a high-μ CMC anneal with an accidental gap. DM checklist: L at I_rms and I_peak; hotspot next to gap reviewed with thermal camera; acoustic whistle checked in light-load modes; interaction with X-caps for filter corner frequencies documented. How CM and DM share a filter—and how to diagnose Typical AC-input π / multi-stage filters: CMC + Y-caps → CM attenuation; DM inductors (or CMC leakage) + X-caps → DM attenuation; sometimes multiple stages for tough industrial / EV limits. Attribute Common mode choke Differential mode choke Current that magnetizes core CM noise / imbalance Load / ripple current Typical nanocrystalline grade High-μ CMC Low/controlled-μ inductor Cap partners Y-capacitors X-capacitors Main risk if wrong grade EMI fail, saturation on imbalance Saturation, heat, whistle Leakage fields Keep low via symmetry Inherent with gaps—manage Diagnostic flow when the scan fails: Does adding X-cap help more than Y-cap (or vice versa)? Points to DM vs CM dominance (with safety limits respected). Near-field probe on CMC vs gapped DM inductor—see open-path EMI signatures for leakage clues. Hot soak retest: ferrite CM parts may fade; nanocrystalline may hold CM impedance better magnetically. Check for mode conversion: poor wiring turns DM energy into CM on the cable. Only then change core materials or AL. Application patterns: EV charger—high line current, hot packaging; nanocrystalline CMC + dedicated DM choke on PFC is common (do not rely on CMC leakage alone). Industrial drives—long motor cables need line-side CMCs; do not double-count EMI and motor-protection inductors. Server PSU—split roles keep thermal and acoustic behavior predictable. Leakage inductance: CMC leakage can provide useful DM inductance in low-power filters. At high current, relying on leakage often means extra copper heating, radiated fields, and uncontrolled tolerance versus a designed DM choke. If you intentionally use leakage, specify and measure it; do not discover it in the EMC chamber. RFQ split language: CMC line: “High-μ nanocrystalline CMC core for CM impedance; target Z/L at ___ kHz; I_rms ___; case temp ___; see CMC selection guide parameters.” DM line: “Inductor-oriented core for DM choke; L at I_peak ___; f_ripple ___; gap policy ___; thermal hotspot limits ___.” Y-capacitors create touch-current / leakage budgets; you cannot endlessly “fix CM” with more Y—that is why CMCs matter. When leakage-current limited, invest in CMC impedance and wiring symmetry before proposing more Y capacitance. After a firmware change that alters light-load behavior, rerun a smoke EMI scan and a quick mic check near DM magnetics before freezing the filter BOM. JH Amorphous supplies CMC-oriented and inductor-oriented amorphous/nanocrystalline OEM cores (ISO9001:2015, IATF 16949)—quote as separate line items. Product starting point: nanocrystalline CMC cores. FAQ Q1: Can one nanocrystalline toroid serve as both CM and DM choke? Not optimally. Different grades and winding intents apply. Some filters use CMC leakage for DM, but high-power designs usually split parts. Q2: Why not use two DM chokes instead of a CMC? Without a CMC, CM impedance often relies on Y-caps and layout alone, which may fail limits or leakage-current budgets. CMCs remain the efficient CM tool. Q3: Does this replace the CMC selection guide? No. This article assigns roles. Use the published CMC selection guide for CMC sizing steps. Q4: Which fails first when grades are swapped? High-μ CMC used as DM → saturation/heat. DM core used as CMC → weak CM impedance and EMI fail. Related reading Common mode choke selection guide (CMC sizing) The μ trap: CMC grade vs inductor grade CMC inductor design: mounts, casing, impedance Nanocrystalline core for common mode choke If you need help splitting CM vs DM magnetics on a filter BOM, contact julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Current Transformer Core Selection Guide: Amorphous, Nanocrystalline, and Accuracy Trade-offs
    Current Transformer Core Selection Guide: Amorphous, Nanocrystalline, and Accuracy Trade-offs
    Sep 29, 2026
    How do you pick amorphous vs nanocrystalline for a CT? Current transformer (CT) core selection starts from measurement or protection purpose, accuracy class, burden, frequency, and maximum current—including fault or inrush peaks that must not saturate the core if accuracy must hold. Amorphous and nanocrystalline cores are widely used in modern CTs because high permeability and favorable magnetics enable compact, low-ratio-error designs compared with older approaches—see also amorphous vs nanocrystalline for EVs/PV—while silicon steel remains common in some line-frequency protective CTs. Nanocrystalline often supports high accuracy and compact measuring CTs; amorphous is frequently chosen for specific cost/performance and protective or dual-purpose designs—always verify magnetization curves, remanence behavior, and temperature drift against your standard (IEC/IEEE accuracy classes). Pick the core for the CT’s accuracy and saturation story, not for CMC brochure μ (μ trap still applies if someone hands you a CMC datasheet). CT roles and material comparison CT intent What “good” means Core selection emphasis Measuring / metering Low ratio & phase error at rated burden High μ, low loss, stable vs temp Protective Accurate enough through fault currents; defined saturation Controlled saturation / remanence per standard Dual-purpose Compromise windows Explicit trade study Electronic / sensing Linearity in used range; SNR Small-signal behavior, noise OEM buyers for EV chargers, industrial drives, energy meters, and SST-like systems should state the intent in the RFQ. A metering nanocrystalline core and a protective CT core are not interchangeable by OD. Ratio error and phase displacement depend on magnetizing inductance (related to μ and geometry), winding resistance and leakage, burden magnitude and power factor, frequency and waveform (harmonics matter in power electronics), temperature, and remanence after asymmetrical faults (especially protection). High permeability reduces magnetizing current, which generally helps measuring accuracy—until remanence or saturation under asymmetrical currents becomes the limiting story for protection classes. Topic Amorphous CT cores Nanocrystalline CT cores Permeability / compactness Strong for many CT designs Very high-μ options; excellent for compact measuring CTs Loss / phase behavior Attractive in many line & mid-frequency uses Excellent for precision measuring in many OEM designs Saturation / remanence Grade & annealing dependent Grade dependent; widely used where high accuracy & size matter Temperature Alloy & finish dependent Alloy Curie ~570°C; finished part still limited by insulation/mechanics Buyer note Ask for magnetization & error curves Ask for error vs current & temp; do not use CMC datasheet alone Exact accuracy is a wound CT result, not a bare core miracle. Core suppliers provide magnetic properties; CT manufacturers validate class. Selection steps and failure modes Fix the standard and class. IEC 61869 family and related metering/protection classes define error limits. Write the class on the drawing before picking ribbon chemistry. Define current range. Rated primary, extended current, and fault levels. If the CT must not saturate at fault, protective requirements drive core area and magnetic knee behavior. Define burden and secondary. Burden resistors or relay inputs change error. Electronic burdens differ from classical relay burdens. Frequency and waveform. Power-electronics currents are not pure 50/60 Hz sine. Harmonics and DC components affect errors and saturation. Test with representative waveforms. Temperature. Automotive and outdoor energy products need −40°C class and hot ambient checks. Validate drift empirically. Mechanical and insulation. Window size for busbar, shielding needs, and hi-pot between secondary and core/case. Saturation and remanence: Measuring CTs optimized for tiny magnetizing current can retain flux after a fully offset fault, delaying accuracy recovery—critical in protection. Designers may use gapped or remanence-controlled cores for some protection classes. That is deliberate magnetic engineering, not a quality escape. Buyer question: “Is this core anneal intended for measuring, protective, or remanence-controlled protective use?” If the supplier cannot say, do not guess from μ alone. Power-electronics environments: Leakage fields from gapped inductors can couple into CT windows. High dv/dt can couple capacitively into secondary wiring—attend to shielding and cable practice. Heat from nearby magnetics shifts CT temperature and error. Place CTs with EMC and thermal maps in hand, not only CAD clearance. Data item Why it matters AL or μ at stated conditions Magnetizing behavior baseline Magnetization / BH related curves Saturation knee understanding Recommended for measuring vs protective Prevents misapplication Temperature notes Drift control Dimensional tolerances Turns and window fit Insulation / coating notes Safety and eddy control Traceability / QMS (ISO, IATF) Automotive & energy OEM needs Production notes: Lot AL sorting when CT designs are sensitive; avoid mixing CMC anneal lots into CT stock; control cutting/gapping if used for remanence control; protect cores from mechanical shock; document winding polarity and shield connections at the CT maker. Accuracy class is earned in process control as much as in alloy choice. If JH supplies cores and a third party winds CTs, freeze: core part number and magnetic grade description; incoming AL sampling plan; handling rules; shield and polarity drawings; final accuracy test ownership. Cite the applicable IEC 61869 (or regional equivalent) parts in RFQs, including extended current ratings and the actual secondary load network for electronic meters. DC components can saturate high-μ cores quickly—state DC presence in the RFQ. Silicon steel CTs remain common in some traditional protective applications; compare size, light-load accuracy, and loss/phase—not only price per kilogram. Dongguan JH Amorphous manufactures OEM/ODM amorphous and nanocrystalline cores under ISO9001:2015 and IATF 16949 and supports CT-oriented discussions separate from CMC high-μ marketing sheets. FAQ Q1: Is nanocrystalline always more accurate than amorphous for CTs? Not always. Many high-accuracy measuring CTs use nanocrystalline successfully, but the finished CT design, burden, and test conditions decide class. Compare curves for your use case. Q2: Can I use a high-μ CMC toroid as a CT core? Sometimes experimenters try; production CT designs need grades and validation aimed at accuracy and remanence behavior. Do not assume CMC stock is CT stock. Q3: How does temperature affect CT error? μ and dimensions drift; copper resistance changes with temperature. Validate across the product temperature range, including cold soak. Q4: What about DC tolerance? DC components can saturate high-μ cores quickly. Hall, fluxgate, or specially designed CTs may be required—state DC presence in the RFQ. Related reading Amorphous vs nanocrystalline selection for EVs/PV How core materials define CMC performance Nanocrystalline core for power applications High-temperature magnetics (temp drift context) For amorphous or nanocrystalline CT core selection against a stated accuracy class, send burden and current profile to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
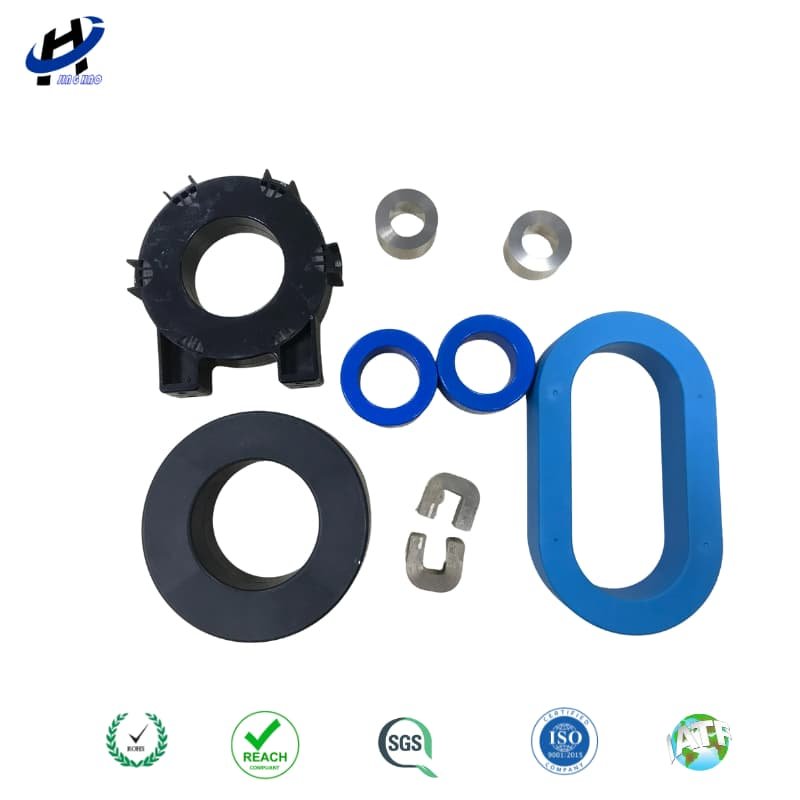
  • Solid State Transformer Magnetic Components Explained: Cores Inside SST Power Stages
    Solid State Transformer Magnetic Components Explained: Cores Inside SST Power Stages
    Sep 28, 2026
    Which cores sit inside an SST power stage? Solid state transformer (SST) magnetic components are the high- or medium-frequency transformers, filter inductors, and EMI chokes that enable power conversion stages to replace bulky line-frequency magnetics. Inside an SST, cores see elevated switching frequencies, multilevel or modular converter stresses, isolation requirements, and thermal density that differ from 50/60 Hz distribution transformers. Nanocrystalline and amorphous alloys often appear in medium-frequency transformers and high-performance filters because of favorable loss/size trade-offs and high Bs (~1.25 T class for iron-based nanocrystalline vs ~0.4 T ferrite), while ferrite remains relevant in some higher-frequency, lower-flux niches. Specify cores by stage function—isolation transformer, link inductor, or CMC—not by a single “SST alloy” slogan. SST magnetics by stage role From a magnetics desk, SST architecture usually breaks into: Input stage — AC/DC or multilevel conversion with line filters (CMCs, DM inductors) Isolation stage — medium/high-frequency transformers (the heart of size reduction) Output stage — inversion or DC ports with additional filter magnetics Auxiliary magnetics — gate-drive transformers, sensors/CTs, snubber inductors Each block has different flux, frequency, and insulation demands. Buying “one core material for the SST” is how programs stall. JH has already published focused content on SST size-versus-heat at 50 kHz and a 24 MW SST nanocrystalline architecture note; here we map component roles and core selection questions so OEM buyers and applications engineers share vocabulary when requesting samples. Isolation / medium-frequency transformer checklist: target frequency band and waveform (square, quasi-square, multilevel); voltage-second product and ΔB budget; isolation voltage, partial discharge, creepage/clearance on the finished winding; thermal path (oil, air, cold plate, potting); mechanical geometry suited to the winding scheme. Material family Typical SST-leaning role Watch-outs Nanocrystalline Medium-frequency isolation & high-performance filters Ribbon insulation, cutting, AL control Amorphous Competitive loss/size in defined bands Noise, cutting, grade selection Ferrite Higher frequency / lower flux designs Temp derating near ~100–120°C class; Bs ~0.4 T Silicon steel Lower frequency / large power traditional Not the SST miniaturization story Nanocrystalline Curie ~570°C helps magnetically at elevated temperature; finished systems still face copper and insulation limits. SST insulation systems may differ from PSU case windows (-40 to +140°C discussions elsewhere) and must be specified explicitly. Filter inductors and link magnetics: Boost / buck / resonant tank inductors depending on topology; DM chokes on AC ports; CMCs for EMI against grid codes. Inductor cores should be inductor-oriented grades with AL vs DC bias honesty—not high-μ CMC grades pressed into energy storage (the μ trap). Gapped designs need fringing hotspot discipline for copper near gaps. Grid-connected SSTs face strict harmonic and EMI expectations. High-μ nanocrystalline CMC grades (often ≈ 80,000–190,000 class) help when high current and strong low-frequency CM impedance are required. Complement—not rewrite—your CMC selection process: size by impedance band, current, and temperature. Cut nanocrystalline C-cores appear in SST isolation and high-frequency transformer stages. Stresses, comparison, and RFQ discipline SST modules may see fast dv/dt from SiC/GaN stressing insulation; common-mode voltages across isolation transformers; uneven module loading in cascaded architectures; wide ambient in outdoor energy cabinets. Core RFQs should include insulation system questions (ceramic vs organic ribbon themes), hi-pot strategy, and thermal mapping—not only Ae and AL. Stage magnetics Primary job Core selection focus Failure if mismatched MF/HF isolation transformer Energy transfer + isolation Loss vs f, ΔB, insulation Overheat, PD, bulk Link / filter inductor Energy storage / ripple AL under bias, fringing Saturation, hot copper Line CMC CM EMI impedance High μ, current, temp EMC fail when hot/loaded CT / sensors Measurement Accuracy, burden, temp Control error Gate-drive transformer Isolation for gates Capacitance, creepage Shoot-through risk Thermal and mechanical: Measure winding and core temperatures under worst multilevel patterns—not only sinusoidal lab excitation. Magnetostriction audible noise can appear in outdoor installations. Vibration in mobile or trailer-mounted systems needs impregnation and mount control. Do not assume liquid cooling of semiconductors cools every magnetic component equally. RFQ template: “Component role: [MF transformer / CMC / DM inductor / CT]. Topology frequency ___ kHz; waveform notes ___; voltage-second or L(I) targets ___; isolation voltage ___; ambient/hotspot ___; cooling method ___; preferred alloy family ___; documentation (ISO/IATF) ___; annual volume ___.” Development sequence: Freeze architecture frequencies and modularity → allocate loss budgets per magnetic component → select materials per role and prototype transformers and filters separately → integrate EMI early (SST cabinets are excellent antennas when leakage is ignored) → only then optimize cost with tooling and PPAP if automotive-adjacent. Skipping EMI early creates late shields and capacitor banks that erase earlier size wins. Appoint a magnetics owner who translates volt-seconds into ΔB and Ae candidates, isolation specs into winding/core insulation asks, cabinet airflow into hotspot limits, and EMC pre-scan results into CMC vs DM actions. In modular SSTs, shared AC-port CMCs see aggregated EMI of many cells—undersizing them is a common system mistake when each cell team only budgets “its own” noise. Tag each BOM line with role and grade family so warehouse staff cannot interchange parts by OD. Dongguan JH Amorphous supplies OEM/ODM nanocrystalline and amorphous cores (ISO9001:2015, IATF 16949) for energy and industrial power electronics teams building SST-like architectures. SST magnetics mix closed toroids and cut cores depending on energy storage vs isolation needs. Filter-stage wound magnetics: size by role (CMC vs DM), not by a single SST alloy slogan. Closed-path toroids for CM filtering alongside cut cores for isolation stages. FAQ Q1: Is nanocrystalline always required for SST transformers? No. It is a strong candidate for many medium-frequency designs, but frequency, voltage, and cooling can favor other families. Compare loss and insulation readiness. Q2: Can ferrite SST transformers work at high power? Sometimes at higher frequency and carefully managed flux/temperature. Bs ~0.4 T and thermal derating near ~100–120°C class behavior limit some dense designs. Q3: Do SSTs still need common mode chokes? Usually yes at AC interfaces and often on other ports. Electronics do not remove EMI physics. Q4: What is the first datasheet trap in SST magnetics buying? Using CMC high-μ permeability rows to specify power inductors or transformers without loss and bias data. Larger core windows for higher power SST stages—loss density and cooling paths dominate sizing. Related reading Engineering the 50 kHz SST size-vs-heat trade-off 24 MW SST design with nanocrystalline cores Amorphous vs nanocrystalline for EVs and PV High-power nanocrystalline cut C-core If you need OEM core samples by SST stage role, email julia@amorphousoem.com with frequency, isolation, and thermal targets — www.amorphousoem.com.
    Read More
  • Automotive Magnetic Core Sourcing: What IATF 16949 and PPAP Mean for Core Suppliers
    Automotive Magnetic Core Sourcing: What IATF 16949 and PPAP Mean for Core Suppliers
    Sep 27, 2026
    What do IATF 16949 and PPAP actually mean for core suppliers? Automotive magnetic core sourcing is not only about AL and OD. IATF 16949 defines the quality management system automotive customers expect from manufacturing suppliers, while PPAP (Production Part Approval Process) is the evidence package that proves a specific core part can be produced consistently at rate. For nanocrystalline and amorphous CMC or inductor cores used in OBC, DC-DC, and traction-adjacent filters, buyers should require system certification, process control on anneal/AL, material traceability, change notification, and a PPAP level agreed in the purchase contract. Dongguan JH Amorphous Co., Ltd. operates ISO9001:2015 and IATF 16949 systems to support OEM/ODM automotive magnetics programs—not catalog hobby parts with an automotive sticker. Why magnetics are special—and what IATF means Soft magnetic cores sit in EMI and power paths that affect homologation and EMC compliance, functional safety indirectly (noise into controllers, sensor CT accuracy), thermal risk next to batteries and power stages, and long field life across -40°C to high cabin/underbody temperatures. A core that drifts AL after an undocumented anneal change can reopen EMC failures months after SOP. Purchasing cannot treat nanocrystalline toroids like generic stampings. Vehicle domain Core roles Buyer pressure points Onboard charger CMC, PFC inductor, DM choke EMI, heat, packaging DC-DC converter CMC, transformers, inductors Wide load, acoustics Inverters / auxiliaries CM filters, sensors Vibration, temp, PPAP EVSE charging equipment Line CMCs, CTs Standards + volume ramp IATF 16949 is an automotive QMS built on ISO 9001 with additional requirements: customer-specific requirements, stronger defect prevention, traceability, and manufacturing process control. For a magnetic core supplier, readiness shows up as: controlled flow from ribbon to anneal to finish to pack; documented work instructions for critical magnetic processes; calibration of AL fixtures and temperature profiling equipment; problem-solving discipline; supplier management for ribbon, cases, and coatings; change control and customer notification pathways. ISO9001:2015 alone is a foundation; automotive OEMs and Tier-1s typically expect IATF 16949 when the part is serial automotive. Onboarding questions: Does the IATF certificate scope cover the manufacturing site that will ship your cores? How are special characteristics defined for AL, dimensions, and insulation? What is the scrap/rework policy on anneal lots that miss μ/AL windows? How are customer-specific OEM requirements flowed down? Can you show process capability thinking on critical dimensions? Automotive-facing coated cores—pair material choice with IATF/PPAP documentation, not brochure μ alone. PPAP for magnetic cores and process risks PPAP is not a single PDF saying “we are good.” Depending on the agreed level, expect: design records / core drawings with tolerances; engineering change documents; process flow diagrams; PFMEA covering anneal, winding-risk interfaces, handling; control plan including AL sampling and visual criteria; MSA on measurement systems; dimensional results; material certifications (alloy, case resin, compliance); performance test results agreed with the customer (AL, impedance samples, hi-pot as applicable); PSW signed. Magnetics-specific reality: magnetic performance must appear in the control plan, not only OD/ID/HT. A dimensionally perfect toroid with wrong anneal is a wrong part. Example special characteristics: AL or μ window at stated conditions; dimensional stack-up affecting winding; insulation coverage / edge condition for gapped parts; case material flammability / markings when specified; traceability code retention. Process step Failure mode PPAP/control focus Ribbon incoming Wrong alloy/insulation lot Certs, traceability Winding core Dimensional, tension damage SPC visuals, capability Anneal / finishing Wrong grade (CMC vs inductor μ) Recipe control, AL gates Gapping Length, burrs, fringing risk Gap metrology, edge Casing / varnish Thermal/mechanical weakness Material UL notes, cure Pack & ship Moisture, deformation Packaging specs The “μ trap”—shipping a high-μ CMC grade when the drawing intended an inductor-oriented low-μ grade—belongs in PFMEA as a mislabel/mis-anneal risk. Automotive validation will exercise cold starts near -40°C class; hot soaks where ferrite may derate near ~100–120°C while nanocrystalline alloy Curie ~570°C holds magnetically (assemblies still limited by copper/case, often discussed -40 to +140°C); vibration and shock; EMC with production harnesses. Bs ~1.25 T class nanocrystalline vs ~0.4 T ferrite often matters for high-current CMCs in OBC filters—see the JHNO71.5 EV CMC core used in a German 800 V case—but PPAP still cares how you keep that performance stable lot to lot. Wound CMC suitable for EV power stages: PPAP cares about process capability as much as AL. Commercial practices that keep programs alive Buyer RFQ should include: application (CMC vs inductor vs CT); electrical targets (L/Z, current, f); environmental targets; annual volume and ramp; PPAP level and customer-specific forms; IMDS / material declaration expectations; packaging and barcode rules. Supplier response should include: proposed grade family and why; preliminary control plan outline; lead time for PPAP samples vs mass production; change notification commitment; contact path for quality and applications (not only sales). Tier-1 coordination: Freeze the magnetic grade name on the drawing—not only “nanocrystalline toroid.” Require PCN for anneal recipe, ribbon supplier, insulation system, and AL fixture changes. Keep golden samples for AL correlation when fixtures update. Align winding houses: gap marks and winding starts affect thermal and EMI. Do not dual-source different anneal philosophies without full requalification. Before full PPAP, screen with: certificate copies with scope pages; example control plan redacted from a similar toroid family; AL histogram from a recent comparable lot; material declaration templates; packaging photo. Dual-source safely means independent PPAP for each manufacturing route, correlated AL fixtures, separate FMEAs, and EMI/thermal delta tests on the finished choke—not only matching OD and “nanocrystalline” text. Dongguan JH Amorphous (www.amorphousoem.com) encourages joint reviews between purchasing and applications engineering so automotive programs do not optimize piece price while breaking EMI. Field context: Italian OBC thermal/EMI case. Production cells where lot traceability and change control feed PPAP evidence packs. Cased CMC cores for OBC/DC-DC: freeze grade and AL windows in the PPAP control plan. Coating and case materials belong in material declarations and change control. FAQ Q1: Is IATF 16949 the same as PPAP approval? No. IATF is the management system certificate for the plant. PPAP approves a specific part/process combination for your program. Q2: Do prototype cores need full PPAP? Usually not at the same level as SOP. Agree interim approval rules for DV samples, then complete PPAP before serial shipments. Q3: Can a trading company provide IATF magnetics? You need manufacturing-site accountability. Ask where anneal and final test occur and whose certificate applies. Q4: What is the most common automotive magnetics sourcing mistake? Buying by OD and μ brochure value without grade intent, AL under bias, and change control—then discovering EMI drift after a quiet process change. Related reading Italian EV charger OEM case study German heavy-duty EV 800 V EMI case JHNO71.5*29.6*30 EV CMC core 800 V OBC/DC-DC magnetics optimization For IATF-aware nanocrystalline or amorphous automotive core quotes, contact julia@amorphousoem.com — www.amorphousoem.com.
    Read More
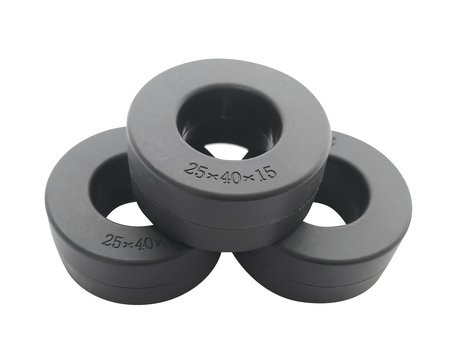
  • Open Magnetic Path EMI Signatures: How Leakage Fields Show Up on EMC Scans
    Open Magnetic Path EMI Signatures: How Leakage Fields Show Up on EMC Scans
    Sep 26, 2026
    How do leakage fields show up on the EMC scan? Open magnetic path EMI signatures appear when flux is not confined inside a high-permeability closed core—because of gapped inductors, poorly canceled windings, rod-like open structures, or leakage from CMCs—and that escaping field couples into cables, PCB loops, and chamber antennas. On EMC scans you often see broadband or harmonic-rich elevations that change dramatically when you move a near-field probe around the magnetics or slightly relocate a harness. Fixing capacitors alone rarely solves it: you need magnetic path control, winding symmetry, layout distance, and sometimes shields—plus the right nanocrystalline or ferrite core strategy for the filter role. Start from the CMC selection guide when the part is truly CM duty. Cased closed-path CMCs: flux stays in the core. Open-path or poorly canceled turns leak onto nearby loops. Closed path vs open path on the bench A toroidal high-μ nanocrystalline CMC aims for a closed magnetic path: common-mode ampere-turns drive flux in the core; differential current largely cancels. An open path (intentional gap, rod core, incomplete cancellation, large leakage) stores or leaks energy outside the core volume. Leakage fields are useful (transformer isolation, some sensors) and harmful (EMI, heating of nearby metal, acoustic vibration). EMC labs see the harmful side as conducted noise that looks immune to Y-cap tweaks, radiated hotspots near magnetics, and failures that appear only with production cable routing. Observation Suggests Near-field probe peaks at gap or rod ends Fringing / open path radiation EMI changes when rotating a toroid CMC Leakage / winding asymmetry Fail band tracks f_sw harmonics Switching magnetics coupling Touching chassis near inductor shifts plot Field into structure currents Cut / gapped cores: the open magnetic path is intentional for energy storage—and it is also where EMI probes light up. CM vs DM roles. CMCs have intentional or parasitic leakage inductance that can help differential filtering—but excess leakage and poor winding symmetry radiate and convert modes. High-μ nanocrystalline CMCs (μ often ≈ 80,000–190,000 for CMC grades) are excellent closed-path CM impedances when wound correctly; they are not automatic EMC insurance if lead dress creates large loops. Gapped DM inductors must leak by design. That fringe is where copper hotspots and EMI pickup coexist—see the fringing loss notes. Treat gap orientation as an EMC orientation problem, not only a thermal one. Reading the scan like a magnetics engineer Identify whether the fail is conducted, radiated, or both. Use a near-field probe map before ordering more capacitors. Correlate peaks to f_sw, burst modes, and PFC harmonics. Temporarily add distance between suspect magnetics and harness—if the plot improves a lot, path/leakage is implicated. Check winding start/finish and twist of CMC leads. Only then change core material, AL, or add shields. This order prevents expensive core swaps when a 20 mm cable move was the real fix. Design controls that reduce open-path EMI Magnetic design. Prefer closed-path CMCs for CM noise; use nanocrystalline when high current + strong low-frequency CM impedance is needed (Bs ~1.25 T class headroom vs ferrite ~0.4 T). For gapped DM parts, minimize unnecessary loop area and keep fringe away from sensitive nets. Avoid treating open rods as filters next to long cables without a shielding strategy. Layout. Short, tight CMC lead pairs. Keep noisy switch nodes away from magnetics that can re-radiate. Mind return paths under inductors on multilayer PCBs. Mechanical. Gap mark orientation standardized in assembly. Metal brackets can be useful shields or accidental shorted turns—validate. System. Cable common-mode chokes at panel entry when cabinet coupling dominates. Keep grounding philosophy consistent with safety and EMC. Ferrite may derate as temperatures approach the ~100–120°C discussion zone; nanocrystalline Curie ~570°C and finished assemblies often discussed from about -40°C to +140°C change the thermal EMI story. Neither material removes the need for closed-path thinking. An open-path ferrite and an open-path nanocrystalline can both fail radiated tests if layout ignores leakage. Dongguan JH Amorphous supports OEM/ODM cores for CMCs and inductors under ISO9001:2015 and IATF 16949. Match closed-path CMC grades vs inductor grades so EMI roles stay clear. Approach When it helps When it fails More X/Y capacitors True CM/DM impedance gaps Leakage coupling / loop antennas Snubbers Switching edges Not a substitute for open-path control Shield cans Local radiated Thermal & capacitive side effects Closed-path CMC upgrade High CM current, hot, LF EMI Wrong if problem is DM gap radiation only Cable routing / twist Harness pickup Ignores on-board fringe Mode conversion. Leakage and imbalance convert differential switching energy into common-mode currents on cables. That is why a “DM-only” inductor problem becomes a conducted CM fail on the LISN. Symmetry, tightly paired returns, and correct CMC placement after the noisy node are essential. Pre-compliance checklist. Photo of gap orientation vs cable exit CMC winding sense and lead length documented Near-field map at f_sw and 2nd/3rd harmonics Hot EMI scan after thermal soak if ferrite is in the path Confirm magnetic grade matches role (CMC vs inductor) Note any metal bracket acting as a turn Change the core when AL, saturation, temperature derating, or CM impedance is truly insufficient Change the drawing when orientation, keep-outs, and lead dress are uncontrolled Wound toroids on the bench: lead dress and proximity to harnesses often move the EMC plot more than another capacitor. FAQ Q1: Does higher permeability always reduce leakage EMI? Higher μ helps confine flux in a closed core for CM magnetization, but winding asymmetry and external loops still radiate. Gapped inductors will always fringe. Q2: Can I use a CMC core as a gapped DM inductor to save SKUs? Magnetically unwise—different grades and purposes. See high-μ vs low-μ datasheet guidance. Q3: Why does my EMI fail only with the production harness? Harnesses form antennas and return paths that lab pigtails omit. Leakage fields need those antennas to show up. Q4: What should I send a core supplier when EMI implicates magnetics? Fail bands, topology, currents, photos of magnetics orientation, and whether the part is CM or DM duty. High-volume casing lines: mechanical consistency of the case also affects leakage and mounting geometry. Related reading Common mode choke selection guide Mastering EMI suppression Air-gap fringing loss (gap radiation / copper) Is common-mode noise sabotaging your circuit? If an EMC plot seems to blame the toroid, send fail bands and magnetics photos to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Ceramic vs Organic Insulation on Soft Magnetic Ribbon: What OEM Buyers Should Ask
    Ceramic vs Organic Insulation on Soft Magnetic Ribbon: What OEM Buyers Should Ask
    Sep 25, 2026
    What should an OEM buyer ask about ribbon insulation? Ceramic-like inorganic and organic insulation systems on soft magnetic ribbon both aim to prevent interlayer eddy loops and turn-to-ribbon shorts, but they differ in temperature endurance, mechanical toughness, thickness, and process windows. OEM buyers should not treat “insulated ribbon” as a single checkbox. Ask what chemistry is used, how thickness and coverage are controlled, what voltage/insulation tests apply after annealing and winding, and how the insulation survives cutting, gapping, and automatic winding. Match the insulation system to temperature class, hi-pot needs, and production method—especially for nanocrystalline and amorphous OEM/ODM cores used in EV, industrial, and energy applications. Why ribbon insulation exists Amorphous and nanocrystalline cores are wound from thin alloy ribbon. If adjacent wraps are electrically shorted over large areas, eddy current paths widen, losses rise, and local heating can damage varnish or enamel on copper windings. Insulation on ribbon (coating, surface insulation, or interlayer dielectric depending on supplier language) reduces conductive contact between wraps while ideally remaining thin enough not to destroy stacking factor. Family (buyer language)Typical characterWhere questions focus Organic / polymericFlexible, process-friendly, thickness trade-offsSolvent, thermal class, long-term aging Ceramic / inorganic-leaningHigher temperature reputation, different toughnessBrittleness, coverage after anneal, dusting Exact proprietary chemistries vary by mill and finisher. Specify performance—breakdown, temperature, adhesion—rather than only a buzzword. Nanocrystalline performance depends on anneal (ribbon flatness and IQC also matter—see ribbon uniformity notes). Insulation must survive thermal profiles used to develop the nanocrystalline structure and the magnetic grade (high-μ CMC vs lower-μ inductor-oriented finishing). Ask: Is insulation applied before or after magnetic anneal (or both in stages)? Does the anneal atmosphere interact with the coating? How is coverage verified after heat treatment? Does cutting for gaps create conductive burrs that bypass insulation? A datasheet line that only says “insulated” without process context is incomplete for automotive-grade risk management. Organic/epoxy-style coatings on nanocrystalline ribbon cores—ask what survives your winding tension and impregnation. Buyer questions and engineering trade-offs Electrical: What interlayer resistance or breakdown method do you use? After winding copper, what hi-pot regimen do you recommend between winding and core? How do moisture and pollution-degree assumptions affect ratings? Thermal: Continuous and short-term temperature limits for the insulation system? Compatibility with impregnation varnish cure temperatures? Behavior in −40°C to +140°C class product environments common to finished nanocrystalline assemblies? Mechanical / production: Does automatic winding abrade the coating? Is there powdering or flaking that contaminates winding machines? How do you handle cut edges on gapped inductor cores? Quality system: ISO9001:2015 evidence; IATF 16949 when automotive? Lot traceability of ribbon + insulation batch? Change-control when the insulation vendor changes? Trade-offs in plain language: Thickness vs stacking factor: Thicker insulation improves dielectric margin but reduces metallic fill, affecting AL and size. Ultra-thin coatings favor magnetic performance but demand process control so pinholes do not dominate yield. Flexibility vs high-temperature reputation: Organic systems often tolerate bending and winding stress better. Inorganic-leaning systems are frequently requested when temperature and long life dominate—yet they must still prove they do not crack at cut edges. Loss impact: Poor insulation raises core loss and temperature, which then stresses the insulation further—a feedback loop visible on thermal cameras as “core hotter than model.” Compatibility: Some impregnants and cleaning solvents attack certain organics. Validate ribbon insulation + wire enamel + varnish + case plastic as one set. Insulation does not replace correct magnetic grade selection. High-μ CMC grades still need proper CM winding and EMI validation. Low-μ inductor grades still need AL vs bias and fringing management. High-temperature capability of nanocrystalline alloy (Curie ~570°C, Bs ~1.25 T class) still requires insulation and case to keep up—pair this with the high-temperature magnetics comparison. Blue-coated family across OD/HT—coating thickness and edge coverage affect interlaminar short risk. Scoring suppliers and RFQ language TopicWeak answerStrong answer Chemistry“Ceramic coated” onlyFamily + thickness target + cure/anneal note Test“We hi-pot sometimes”Method, sample size, fail criteria Heat“High temp OK”Limits tied to product ambient/hotspot Edges“No problem”Cut-edge procedure for gapped parts Change controlInformalPCN path, especially IATF customers Paste-ready RFQ language: “Soft magnetic ribbon shall include interlayer insulation suitable for [automatic/hand] winding. Supplier shall state insulation family (organic/inorganic), nominal thickness or stacking-factor impact, anneal compatibility, recommended hi-pot between winding and core, and edge treatment for gapped cores. Lot traceability required. Automotive programs require IATF 16949 and PPAP per agreement. Compliance: RoHS/REACH; UL where applicable to case/insulation systems.” Incoming IQC metrics when voltage stress or automatic winding matters: visual coverage uniformity; edge condition after cutting; abrasion trial on a short winding spike; occasional interlayer resistance sampling; contamination check for flaking in the tray. Run a short pilot lot before freezing the insulation callout—hand-wound prototypes can pass a coating that sheds under production tension. Require PCNs for insulation system changes—especially on IATF 16949 automotive programs. Dongguan JH Amorphous aligns OEM/ODM supply with ISO9001:2015 and IATF 16949 expectations and supports RoHS/REACH documentation pathways. Ask for the declaration set early in tooling, not after pilot EMI. Field failure patterns linked to insulation: gradual efficiency loss as interlayer shorts progress; sudden hi-pot failure after thermal shock; localized burn at cut gap edge; winding-machine contamination alarms. Each should trigger a materials review, not only a copper wire diameter change. Bead/sleeve coated parts: insulation must survive automatic winding without nicking the ribbon. FAQ Q1: Is ceramic insulation always better than organic? No. “Better” depends on temperature, flexibility, thickness budget, and proven process control. Many successful OEM cores use organic systems when validated. Q2: Can insulation fix a wrong magnetic grade? No. It will not turn a high-μ CMC core into a DC-bias-stable power inductor. Q3: Do I need insulation on ferrite cores the same way? Ferrites are sintered ceramics, not wound ribbon; interlayer ribbon insulation is a wound-ribbon topic. Ferrite has its own coating practices for corrosion and creepage. Q4: What failures look like when insulation is inadequate? Higher than expected core loss/heat, burn marks at edges, intermittent hi-pot fails, and sometimes EMI changes if impedance drifts with temperature. Related reading High-temperature magnetics: ferrite vs nanocrystalline Nanocrystalline ribbon uniformity and high-frequency reliability Nanocrystalline CMC core product family Vacuum heat treatment / anneal quality control If you are writing an RFQ and need clear ribbon-insulation ask items, send winding process and hi-pot targets to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • High-Temperature Magnetics: When Ferrite Derates Near 100°C and Nanocrystalline Holds
    High-Temperature Magnetics: When Ferrite Derates Near 100°C and Nanocrystalline Holds
    Sep 24, 2026
    When does ferrite fall off and nanocrystalline still hold? High-temperature magnetics fail in two ways: the core’s permeability and saturation collapse as you approach the material Curie region, and the winding/case system exceeds insulation or solder limits. Mn-Zn ferrite commonly used in SMPS CMCs and transformers shows strong parameter derating in the ~100–120°C neighborhood familiar to power engineers, because its Curie point sits relatively low. Iron-based nanocrystalline cores, with Curie ~570°C and typical finished-case conversations often spanning about −40°C to +140°C, hold usable magnetic performance deeper into hot ambient and hot-spot maps—provided copper, plastics, and varnish are rated accordingly. Choose material by the real hottest-spot budget, not by room-temperature AL alone. Temperature stack and material comparison Datasheets quote ambient; failures happen at the hottest local temperature. A realistic stack for an EV charger OEM or industrial drive maker: Ambient air or coolant inlet Enclosure / cold-plate interface rise Core surface / case temperature Winding hotspot (often higher than core average) Nearby power semiconductors adding heat Ferrite vs nanocrystalline debates that only compare 25°C μ miss items 3–5. A ferrite CMC that meets insertion loss on a cool bench can lose impedance after soak in a sealed IP-rated box—the same pattern as our Italian 22 kW OBC case and German 800 V heavy-duty filter case. ParameterMn-Zn ferrite (typical CMC/transformer)Iron-based nanocrystalline Bs near room temp~0.4 T~1.25 T Curie temperatureRelatively low (watch ~100–120°C class derating)~570°C Finished core/case windowOften limited by μ/Bs collapse + plasticOften discussed −40°C to +140°C for cased parts Design implicationUpsize or relocate when hotMagnetic headroom remains; manage copper/plastics Why ferrite falls off near 100°C: As temperature rises toward its Curie region, Bs drops; permeability can rise then collapse depending on grade; inductance and impedance targets drift; saturation risk under the same ampere-turns increases. Designers compensate with larger cores, more parallel paths, forced air, or relocating the filter—each costly in automotive and dense industrial racks. Symptoms of thermal magnetic derating: EMI that passes cold and fails after thermal soak; inductor current distortion that worsens when hot; protection trips on inrush only at elevated temperature. Always correlate with thermocouples on the core case and winding, not only chamber air. Why nanocrystalline holds magnetically hotter: High Bs (~1.25 T class) for ampere-turn headroom; Curie ~570°C so the alloy is not near magnetic death at 120–140°C case temperatures; high-μ CMC grades (often ≈ 80,000–190,000 class) that keep CM impedance strong when ferrite has already surrendered margin. The limiting parts of a nanocrystalline choke at high temperature are frequently enamel and interlayer insulation, case polymer continuous-use temperature, solder joints, and copper resistivity rise. “Nanocrystalline holds” means the magnetic function holds; thermal design of the assembly remains mandatory. Cased nanocrystalline cores for elevated ambient—case and ribbon insulation share the thermal budget with copper. Where the decision bites and how to select Automotive OBC / DC-DC: Wide ambients; IATF 16949 sourcing expects temperature qualification. Nanocrystalline CMCs—see the JHNO EV CMC core family—are common when high current and hot EMI filters coincide. Industrial drives and PV inverters: Cabinet hotspots above ferrite comfort zones appear near heatsinks and reactors. A material swap can restore EMI margin without enlarging the cabinet cutout. Server / telecom PSU: Airflow is planned, but filter corners can still stagnate. Liquid-cooled platforms keep semiconductors happy while magnetics on the warm side of a cold plate still run hot—do not assume liquid cooling cools every toroid. Selection process: Map the hotspot with sensors at worst airflow. Translate: Is the failure μ/Bs collapse (ferrite story) or copper/insulation (assembly story)? Pick candidates: ferrite only if hotspot stays in its comfortable band; nanocrystalline when magnetic derating is the limiter. Re-size copper for resistivity at temperature; check rise again. Qualify cold too (−40°C class for automotive). Document derating curves for PPAP/DFMEA when automotive. Decision factorStay with ferriteMove to nanocrystalline Hotspot modest, current modestOften OKOptional Hot EMI fail after soakRiskyStrong candidate High CM current + tight copperDifficultStrong candidate Cost-only cool consumer SMPSOften winsMay be overkill Automotive wide-temp + IATFPossible with careFrequently preferred for CMC Test notes: Soak at temperature with power, not only oven preheat then quick test. Measure impedance/insertion loss hot when EMI is the requirement. For inductors, measure L vs I hot. Include humidity/bias if insulation resistance matters. Watch acoustic behavior hot and cold—damping changes. Piece-price alone before thermal EMI failures is the wrong metric. Count validation days, shielding/capacitor overdesign, field-return risk, and cabinet volume. High-temperature magnetics is a system cost problem. Dongguan JH Amorphous (www.amorphousoem.com) manufactures OEM/ODM nanocrystalline and amorphous cores with ISO9001:2015 and IATF 16949 systems and helps buyers separate alloy capability from case/wire limits in RFQs. Assorted cased CMC sizes used in EV and industrial filters where ferrite μ has already rolled off. FAQ Q1: Does nanocrystalline never need derating? It needs assembly derating. The alloy’s Curie (~570°C) is high, but wire, case, and PCB still limit continuous temperature. Typical finished-case discussions often reference about −40°C to +140°C depending on construction. Q2: At what temperature should I stop using ferrite CMCs? There is no single universal cutoff. When measured core temperature enters the zone where the chosen ferrite’s Bs/μ curves fall off sharply (often discussed near ~100–120°C class behavior), redesign or material change is warranted. Q3: Will a bigger ferrite always fix heat derating? Sometimes, at the cost of volume and copper. If ambient already sits near the ferrite problem region, size alone may not restore margin efficiently. Q4: What data should I request from a core supplier? Temperature-relevant AL or impedance notes, recommended case materials, insulation options, and automotive documentation path (IATF/PPAP) when needed. Larger assemblies still rely on the same nanocrystalline Curie margin versus ferrite near 100°C. Related reading Italian EV OBC thermal & EMI case (54 mm nano) German 800 V heavy-duty EV EMI case (JHNO71.5) JHNO EV CMC core product page Why traditional ferrite chokes fail at high frequency If EMI or inductance drifts after thermal soak, share hotspot temperatures and filter targets with julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Air-Gap Fringing Loss: Why Copper Hotspots Sit Next to the Gap (and How to Place Windings)
    Air-Gap Fringing Loss: Why Copper Hotspots Sit Next to the Gap (and How to Place Windings)
    Sep 23, 2026
    Why is the copper next to the gap always the hotspot? Air-gap fringing loss appears when the magnetic field bulges out of a discrete gap and cuts nearby copper, inducing extra eddy-current heating. That is why thermal cameras often show winding hotspots immediately adjacent to the gap—even when average current density looks safe. Reduce the problem by keeping copper out of the strongest fringe, using spacer/coil architectures that distance the first turns, considering distributed or carefully shaped gaps, and verifying both loss and inductance under DC bias. Material choice (ferrite, amorphous, nanocrystalline) still matters for Bs and temperature, but winding geometry next to the gap frequently dominates local hotspots. Why fringing exists and where it heats An air gap stores energy by lowering effective permeability and linearizing AL under DC bias. The field does not stop abruptly at the gap edges: flux fringes into the winding window. Consequences: local H and B outside the intended gap volume; AC field components cutting copper strands → eddy losses that scale badly with frequency and strand diameter; proximity-effect aggravation in nearby layers; mechanical forces that contribute to acoustic noise. For OEM power inductors in PFC stages, DC–DC bricks, and differential-mode chokes, fringing is everyday gapped design—not a corner case. LocationWhy it runs hotMitigation theme Turns hugging gap facesStrongest fringe cuts copperKeep clearance; use slot bobbins Inner layer near gap on cut toroidConcentrated bulgeOffset winding, spacer Thick Litz bundle in fringeStrand eddySmaller strands, move bundle PCB copper under gapped ER/PQField into planeCutouts, distance Fringing loss vs classic copper I²R: Design reviews sometimes blame “not enough copper” when IR drop is fine but the hotspot is brutal. Split the budget: (1) DC I²R from I_rms and resistance; (2) skin and proximity in the winding volume generally; (3) fringing-induced eddy localized where gap flux escapes. Item (3) can dominate a small region, raising local temperature enough to discolor enamel while average winding rise looks acceptable. Rule-of-thumb notes (refine with FEA or experiment): fringing influence extends on the order of the gap length into the window—treat “several gap lengths” as a keep-out intuition. Higher f_sw and larger strand diameter in the fringe make eddy heating worse. Increasing gap to hold L under bias can improve magnetic linearity yet worsen fringe heating—trade explicitly. Nanocrystalline and amorphous gapped cores used for high-current inductors—including PFC inductor cores—can run substantial AC flux. Bs headroom (~1.25 T class for iron-based nanocrystalline vs ~0.4 T ferrite) helps size, but copper next to the gap still needs respect. Treat core shape and gap method as the technical distinction—not casual shape nicknames. Cut C-cores make the gap explicit: fringing fields leave the cut faces and heat nearby copper. How to place windings on gapped cores Cut / gapped toroid: Identify gap location on the finished core. Leave a copper-free sector around the gap when the design allows. Start winding away from the gap; use tape or spacer to enforce distance. Prefer Litz appropriate for f_sw, but do not park a thick bundle in the fringe to fill the window. For production, document winding start angle relative to the gap mark so every operator repeats the thermal result. Bobbin cores (PQ, E, ER): Use coil geometries that recess the first winding layer from the gap centerline. Watch foil windings: wide foils are efficient for DC but can act as eddy sails in fringe—slotting or distancing may be required. Thermal vias and potting help only if heat can leave; they do not remove the eddy source. Distributed gap approaches: Distributed gaps reduce peak fringe intensity compared with one large discrete gap, often improving copper temperature at the cost of different loss and cost structures. Evaluate on your f_sw and current; do not assume “distributed always cooler” without measurement. Dongguan JH Amorphous supplies OEM/ODM nanocrystalline and amorphous cores (ISO9001:2015, IATF 16949). For inductor grades we emphasize AL vs DC bias, loss orientation, and manufacturing marks that help winding houses avoid the gap hotspot. Product mix showing cut cores beside closed toroids—gap policy belongs in the RFQ, not as an afterthought. Design workflow and production drift Set L(I) requirement—define I_sat and I_rms. Choose gap / effective μ strategy—discrete vs distributed. Estimate copper loss without fringe; then add experimental margin or FEA for the gap region. Prototype with a thermal camera focused on gap-adjacent copper. Iterate winding distance and stranding before enlarging the core as a first move. Re-check EMI and acoustics—gap and winding changes affect leakage and noise (and can feed inductor whistle if ΔB sits in the audio band). LeverProsCons Increase clearance to gapFast, low tooling costMay reduce turns window Finer Litz in fringe zoneCuts eddy in hotspotCost, fill factor Split/distribute gapLower peak fringeProcess complexity Larger AeLower ΔB & densitySize, cost, weight Lower f_swLess AC eddySystem-level impacts The cheapest watt saved is often a few millimeters of winding offset. Control-plan items for gapped cores: gap length tolerance; visual gap mark relative to case; AL window at stated DC bias points; ribbon insulation integrity after cutting; cleanliness (metal fines must not bridge turns). Prototype-to-mass drift: hand-placed spacers omitted later; Litz strand diameter change; varnish change; clamp force shifting copper into the fringe; firmware raising f_sw without revisiting fringe eddy. After a thermal fix, re-run conducted EMI and update the BOM so purchasing cannot “equivalent” a core with a different gap-mark scheme. Cased closed cores avoid discrete gaps; when you do gap, plan winding clearance for fringing hotspots. FAQ Q1: Does fringing change the effective inductance? Yes. Fringing increases effective gap area somewhat, raising AL slightly versus a naïve gap formula. Calibrate AL on the real core. Q2: Are nanocrystalline gapped cores worse for fringing than ferrite? Fringing is geometric. Nanocrystalline’s higher Bs can shrink size and raise field density if you push miniaturization, which can intensify local problems—design responsibly. Q3: Can I shield the gap with copper tape? A shorted shield in the fringe can itself heat and may alter inductance. Use carefully and measure; it is not a free thermal fix. Q4: What should RFQs include? Gap specification, AL vs bias, preferred winding keep-out, f_sw, I_rms/I_peak, and a request for gap location marking for manufacturing. Related reading Why power inductors whistle (magnetostriction) The μ trap on nanocrystalline datasheets Amorphous cores for PFC inductors Nanocrystalline cores for power applications If a thermal camera shows copper hot next to the gap, send gap length, f_sw, and current targets to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • Why Your Power Inductor Whistles: Magnetostriction vs Thermal Noise in Soft Magnetic Cores
    Why Your Power Inductor Whistles: Magnetostriction vs Thermal Noise in Soft Magnetic Cores
    Sep 22, 2026
    Is that whistle magnetostriction or something else? A power inductor “whistle” is usually audible magnetostriction or mechanical vibration driven by magnetizing force at audio-band frequencies—not random thermal hiss. Soft magnetic cores strain slightly with flux (magnetostriction). If drive frequency, harmonics, or beat notes fall near 2–20 kHz, the assembly radiates sound. Thermal effects change expansion and varnish damping; they rarely create a pure tone alone. Fix the root: reduce ΔB in the audio band, avoid discontinuous magnetizing patterns that create tones, damp the mechanical stack, and select inductor-oriented grades (nanocrystalline or amorphous) with noise and loss in mind—not only AL and Bs. Diagnose before you swap the core Field returns that say “the magnetics sing” mix several mechanisms: Magnetostrictive acoustic emission — dimensional change with B, coupling into case, PCB, and chassis. Lorentz / winding forces — conductors in leakage fields vibrate at twice line frequency or at switching-related tones. Mechanical buzz — loose gaps, clips, varnish voids, or mounting resonance. True thermal (Johnson) noise — broadband and tiny; almost never the tonal whistle heard across a lab bench. SymptomLikely dominant causeFirst checks Pure tone tracking f_sw or f_sw/NMagnetostriction / magnetic forceΔB, DCM/CCM boundary, burst mode Tone at 100/120 Hz or multiplesLine-frequency magnetics / LorentzRectifier ripple, mounting, clamps Rattle changing with tap testLoose mechanical stackGap filler, varnish, clip torque Broadband hiss, no loud toneElectrical noise / EMI pathNot a core whistle problem Replacing a core “because it is noisy” without checking excitation frequency and mounting often moves the tone instead of removing it. Physics that matters for buyers: sound power scales with flux swing and mechanical coupling, not with μ alone. Burst-mode, skip-cycle, and light-load regimes often push energy into audible bands even when full-load operation is quiet. Gapped inductors add fringing; fringing increases local copper force and vibration paths next to the gap. Case, epoxy, and mounting can damp or amplify. Iron-based nanocrystalline materials offer Bs ≈ 1.25 T and usable temperature windows that support compact designs. Compactness raises ΔB if turns and Ae are pushed hard. Noise control belongs in the magnetic design review, not only in the enclosure review. FactorMn-Zn ferriteAmorphousNanocrystalline Bs (typical order)~0.4 THigh (alloy-dependent)~1.25 T Audible risk driverΔB & burst modesMagnetostriction + mountingMagnetostriction + high ΔB if over-miniaturized High-temp holdDerates near ~100–120°C classApplication-dependentCurie ~570°C; finished cases often −40 to +140°C Design leverLower ΔB, avoid burst tonesDamping, grade, impregnationGrade/finishing, ΔB, impregnation, mount No material is always silent. Excitation and mechanics dominate. Copper on a toroid can couple magnetostriction into audible vibration—diagnose before you change the core chemistry. Thermal–mechanical effects vs “thermal noise” “Thermal noise” in electronics usually means Johnson noise—irrelevant to a whistling choke on a bench. What people often mean: Temperature-driven dimensional change altering clamping force and resonance Varnish Tg / softening changing damping as the inductor warms Differential expansion between copper, core, and plastic case creating buzz after soak Those modulate an existing magneto-mechanical drive. They do not replace magnetostriction as the tone generator. Cold start: stiff varnish, higher mechanical Q → sharper tone possible. Warm operation: damping may rise or fall with the resin system. Hot spot near a gap: local copper expansion and force concentration. Automotive cold (−40°C class) vs under-hood heat: mount stiffness changes. Spec acoustic checks at min, typical, and max temperature—not only at 25°C lab air. Coated power-inductor toroid: coating and case stiffness change how vibration reaches the PCB. Design levers that cut whistle Magnetic excitation: Prefer continuous conduction strategies that avoid audio-band burst patterns when product requirements allow. Reduce ΔB with more turns, larger Ae, or lower voltage-second product. Spread spectrum or shift frequencies out of peak ear sensitivity only when EMI and control allow—then revalidate EMC. Avoid operating near saturation corners where magnetizing-current distortion creates strong harmonics. Select inductor-oriented grades (controlled effective μ under bias)—not a high-μ CMC core pressed into energy-storage duty (μ trap explained). Core finishing and mechanics: Discuss impregnation, varnish, and case damping with your core OEM. For gapped parts, treat the gap region as both a thermal and acoustic hotspot—see also air-gap fringing loss and winding placement. Use rigid, damped mounting; avoid cantilevered heavy magnetics. Potting can damp vibration but may raise thermal resistance—validate both. Lab sequence: Capture inductor current and a microphone channel on the same DAQ. Sweep load from no-load to full, including firmware modes sales demos never show. Note core-case and winding temperatures. Repeat with a soft pad under the board to separate structure-borne contribution. Change one magnetic variable at a time (gap, turns, grade, varnish). EV charger light-load night charging and server acoustic contracts are common failure contexts: burst PFC or LLC skip modes create household-audible tones even when full-load EMI passes. Ask for light-load acoustic acceptance in the DV plan. Dongguan JH Amorphous supports OEM/ODM nanocrystalline and amorphous cores under ISO9001:2015 and IATF 16949. We do not promise a universal silent alloy; we match grade, AL under bias, and finishing to your excitation and mounting reality. Epoxy-coated nanocrystalline rings used in inductor and CMC builds where acoustic limits matter. FAQ Q1: Is magnetostriction the same as core loss? No. Core loss is energy dissipated as heat from hysteresis and eddy currents. Magnetostriction is strain. They can correlate with excitation, but fixing loss does not automatically fix sound. Q2: Will a higher-μ nanocrystalline core whistle less? Not necessarily. Higher μ may reduce turns for a target L at low bias, but a CMC-oriented high-μ grade used as a power inductor can worsen harmonics via saturation. Match grade to inductor duty. Q3: Can thermal noise explain a loud 6 kHz tone? Almost never. A loud pure tone is magneto-mechanical or mechanical. Thermal noise is broadband and tiny. Q4: What should I put on an RFQ if acoustics matter? State max SPL or “no audible tone at 1 m in quiet room” across load/temperature, list firmware modes, and request inductor-grade cores with impregnation options—not only OD and AL. Related reading Air-gap fringing loss and winding placement The μ trap: high-μ CMC vs low-μ inductor grades High-temperature magnetics comparison PFC inductor amorphous cores If a prototype inductor is whistling and you want a second look at grade and excitation, send I_L / V notes to julia@amorphousoem.com — www.amorphousoem.com.
    Read More
  • The μ Trap on Nanocrystalline Datasheets: High-μ CMC Grades vs Low-μ Power Inductor Grades
    The μ Trap on Nanocrystalline Datasheets: High-μ CMC Grades vs Low-μ Power Inductor Grades
    Sep 21, 2026
    Why does datasheet μ keep sending the wrong core? Nanocrystalline datasheet permeability is not one number for every design. High-μ CMC grades (μ ≈ 80,000–190,000) are finished for common-mode impedance with minimal intentional gap. Low-μ power inductor grades use controlled shear, gap, or process tuning so L stays linear under DC bias. Swap the grades and you get early saturation, wrong AL, whistle, or EMI fail. Read Bs (~1.25 T iron-based nano), μ or AL at stated frequency and excitation, DC-bias curve, and temperature notes before freezing the BOM. Match grade to function first; size second. Why datasheet μ misleads Most RFQs arrive with a μ screenshot and a target L. That looks efficient—and incomplete. μ on a nanocrystalline datasheet is usually measured on a specific test geometry, at low AC excitation (often millitesla), at a stated frequency (commonly ~10 kHz), and without the DC bias your power stage applies. A “μ = 90,000” CMC row can be true at small signal and still useless for a PFC boost inductor at several amperes DC. A controlled low effective-μ inductor grade—often discussed in the ~200–600 range for some power inductor families, grade-dependent—can look weak next to a CMC sheet until you overlay the bias curve. Then L holds where the high-μ part has already collapsed. At Dongguan JH Amorphous we see this weekly from EV charger, industrial drive, and server PSU teams (same failure mode as our Italian OBC and German 800 V filter cases): the mechanical drawing matches, the ribbon chemistry is nanocrystalline, yet the finished choke fails because the magnetic grade was chosen from the wrong column. IntentFinishingOptimizeFailure if mismatched CMCHigh initial μ, closed pathZ_cm over EMI band, few turnsSaturates on imbalance; EMI collapses Power / DM inductorLower effective μ via process/gapAL under DC bias, linear LExcess Im, hot copper, whistle CT / sensorAccuracy-oriented gradeRatio/phase error, temp driftMetering error, mis-trip “High” and “low” are relative to the envelope, not a ranking. High-μ CMC grades usually ship as closed-path cased toroids—read μ with the finishing route, not as a universal ranking. High-μ CMC vs low-μ inductor grades High-μ CMC typical ranges we support: Bs ≈ 1.25 T (Mn-Zn ferrite ≈ 0.4 T); initial μ often ≈ 80,000–190,000; finished case window commonly −40°C to +140°C; Curie ≈ 570°C—so thermal μ collapse is not the ferrite near-100°C story. How to read a high-μ row: confirm measurement frequency (EMI cares about impedance from ~150 kHz up); ask for AL (nH/N²), not only μ; request DC-bias or imbalance notes; check casing and ribbon insulation for automatic vs hand winding. High-μ is the right tool for broadband CM impedance at high line current with limited copper budget. It is the wrong tool for storing energy under DC bias. Low-μ / inductor grades deliberately reduce effective μ so the B–H loop stays usable under ampere-turns, ½LI² is predictable, and fringing can be managed by gap/process choices. Comparing that μ to a CMC datasheet without the bias column makes the inductor grade look inferior. In the power stage it is often superior. Inductor checklist: AL vs DC bias at I_peak and I_rms; core loss density at f_sw and ΔB; fringing/hotspot guidance if discrete gap; magnetostriction risk in the audio band; thermal derating of copper and case, not only Curie. Rule of thumb: if the part must store energy or hold L under DC, start from the inductor-grade family and verify bias. If it must present CM impedance with canceling ampere-turns, start from the high-μ CMC family and verify EMI-band impedance. ParameterHigh-μ CMCLow-μ inductor Small-signal μ / ALVery highModerate / controlled First useCM EMI chokePFC / DM / energy storage DC bias toleranceSaturates earlier in ampere-turnsDesigned to hold L under bias Risk if swappedInductor saturates; overheatingCMC underperforms; EMI fail One OD for both roles is fine only after both grades are qualified on their own curves. Wound CMC example: ampere-turn cancelation depends on the high-μ grade; the same OD in an inductor finish behaves differently under DC bias. How OEM buyers should spec permeability Replace “need μ > 80k” with a function-led RFQ. CMC cores: application (1-phase / 3-phase / DC); target Z_cm or L_cm at stated frequency points; I_rms, I_peak, expected imbalance; ambient/case target; OD/ID/HT, case material, UL/RoHS; preferred AL range plus impedance or sample insertion-loss data. Power inductor cores: topology and f_sw; L at I_sat and I_rms; ΔB / loss budget; acoustic limits if any; gap policy and winding window; preferred AL vs DC bias plus loss data. Questions that expose the trap early: Is this quoted from a CMC finishing route or an inductor route? At what H (or ampere-turns) was μ measured? Do you have AL at my DC bias? Is ribbon insulation rated for my winding process? Practical notes: high-μ permeability still falls with frequency—use impedance vs frequency of the wound choke. High μ reaches a given B with less H, so unintended DC can saturate a CMC earlier than a lower-μ part of similar Ae. Ask for lot AL tolerance and sort method on OEM builds. Coated nanocrystalline family—match AL / bias / impedance curves to the function column on the datasheet. FAQ Q1: Is higher nanocrystalline datasheet permeability always better? No. Higher μ helps common-mode chokes that need high L with few turns at low bias. Power inductors usually need controlled lower effective μ so inductance survives DC bias. Q2: Can one nanocrystalline toroid OD serve as both CMC and inductor? Mechanically sometimes; magnetically only if you select the correct finishing grade for each role and qualify both. Sharing OD without sharing grade is how the μ trap enters the BOM. Q3: What permeability range should I request for a high-current CMC? Many high-μ CMC grades fall around ≈ 80,000–190,000 depending on grade and test conditions. Confirm AL, bias behavior, and impedance vs frequency rather than locking a single brochure μ. Q4: Why does my inductor get hot when I used a high-μ nanocrystalline core? Likely early saturation under DC ampere-turns, excess magnetizing current, and copper loss—sometimes plus fringing if gapped. Move to an inductor-oriented grade and re-check AL vs bias and loss. Related reading Common mode choke selection guide Nanocrystalline CMC cores for EV power units High-temperature magnetics: ferrite vs nanocrystalline Mastering EMI suppression with common mode chokes If a datasheet μ row looks ambiguous for your CMC or inductor RFQ, email julia@amorphousoem.com with topology, current, temperature, and target L or Z_cm — www.amorphousoem.com.
    Read More
1 2 3 4

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

home

products

WhatsApp

Contact